Manufacturing

Addressing Torsion Issues on a Fiber Ribbone Line

Could the machines manufacturing fiber optic cable production machinery be the unseen force that ultimately delivers true gigabit access to every American home? This article delves into the recent breakthroughs in FTTH Cable Production Line Technology. These advancements are reshaping broadband network infrastructure and accelerating fiber to the home technology across the United States.

FTTH Cable Production Line

Fiber Secondary Coating Line

Compact Fiber Unit

Modern advancements in automation, precision engineering, and AI-driven inspection are significantly reducing production costs and improving quality. This synergy makes high-speed internet technology more trustworthy and simpler to deploy for service providers and municipalities.

Global optical cable output now exceeds hundreds of millions of kilometers annually. This surge is driven by 5G deployments, hyperscale data centers, and the growing demand for streaming and remote work. The subsequent sections will cover automation and Industry 4.0, the use of low-loss materials, AI quality control, innovative cable designs such as bend-insensitive fiber and flat drop microcables, and the pursuit of sustainability in production lines.

Telecommunications manufacturing, network planning, and procurement professionals will discover valuable insights. These insights focus on selecting the right fiber optic cable production machinery and optimizing processes. They are designed to meet regional deployment needs and future bandwidth growth.

FTTH Cable Production Line Technology

The term encompasses the machinery, control systems, and materials transforming optical preforms into deployable fiber cables. It encompasses fiber drawing and coating, SZ stranding, ribbon formation, extrusion of jackets, armoring, taping, automated testing, and final take-up systems. Each step’s precise control defines the fiber optic cable production process, ensuring consistent performance.

The manufacturing chain demands stringent tolerances. SZ stranding systems align dozens of strands with micron-level tension precision. Extrusion lines employ servo-driven extruders and laser micrometers to maintain jacket thickness within ±0.02 mm. Such precision minimizes variability, reducing attenuation and simplifying splicing in the field.

Standards and regulatory frameworks significantly influence manufacturing decisions. Compliance with ITU-T recommendations, such as G.657, and regional fire codes like CPR in Europe, is essential. Meeting these standards ensures products align with the broader broadband network infrastructure.

Quality in production directly impacts network economics and service delivery. Lower attenuation and consistent geometry reduce splice loss and extend reach. This enhances reliability for carriers, ISPs, and utilities, while lowering the total cost of ownership for FTTH deployments. The growing demand for symmetrical multi-gigabit services, 5G backhaul, and data center interconnect is driving the scale-up of modern lines.

Comparing key process components and tolerances reveals their impact on output and quality.
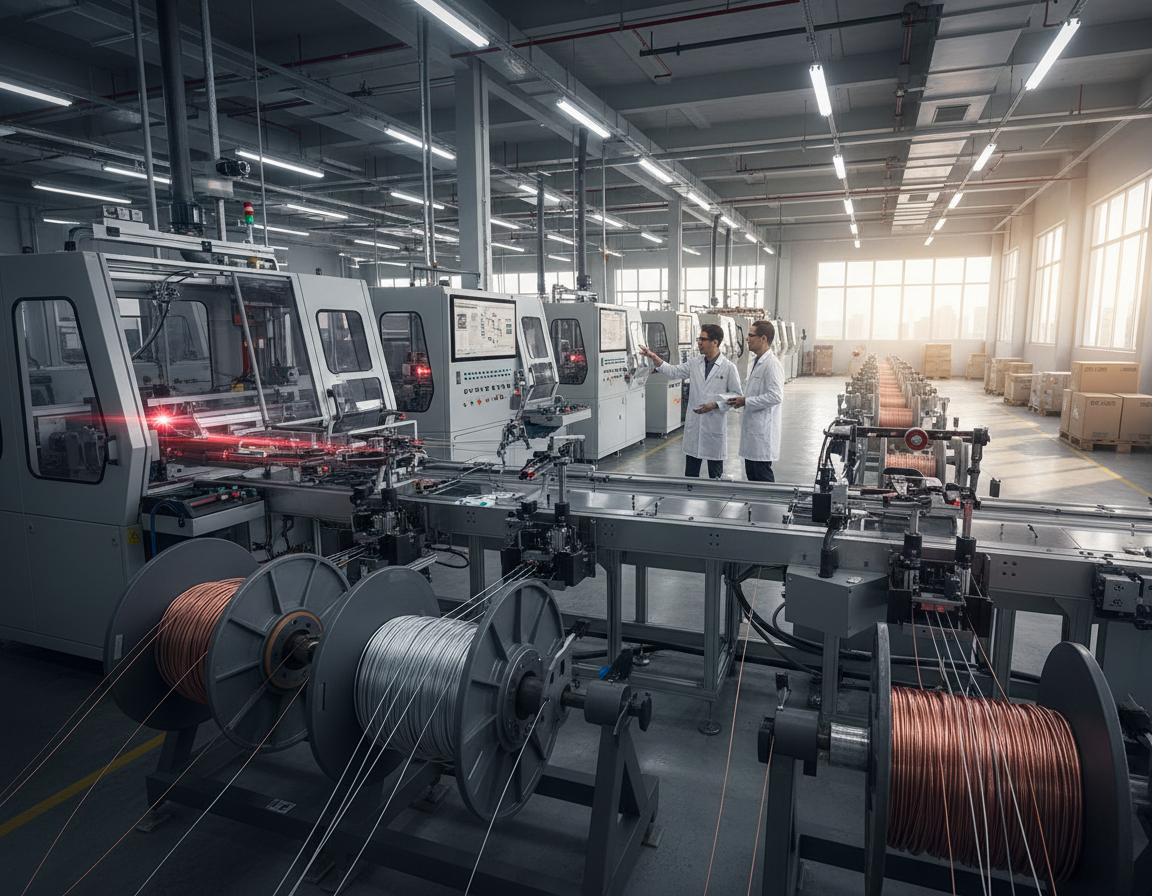
SZ Stranding Line

Production Component Standard Control Performance Impact
Fiber draw and coating Temperature stability ±1°C; concentricity control ±5 µm Stable fiber profile; lower bending-related loss
SZ stranding & ribbon formation Tension control at micron scale; synchronization to 0.5 ms Consistent fiber pitch; reliable splice and connector behavior
Extrusion and jacket thickness Laser-based feedback; ±0.02 mm thickness control Reliable mechanical protection; consistent installation response
Armoring & taping Servo feed rate; layer alignment control Better crush resistance; meets aerial and underground specs
Automated testing and take-up OTDR and insertion-loss verification at production speed; controlled winding tension Complete quality traceability; lower rework and fewer failures in the field

Manufacturers like Corning, Prysmian Group, and Sumitomo Electric focus on tighter process control to meet operator expectations. Continuous advancements in the fiber optic cable production process enable networks to scale while maintaining performance in the last mile of broadband network infrastructure.

Automation And Industry 4.0 In Fiber Optic Cable Production

Factory floors for fiber optic cable production machinery now mirror advanced manufacturing plants from other industries. Smart controls, synchronized stages, and data-driven decision making raise output and protect quality. These shifts shorten commissioning time for new product families. They let telecommunications equipment manufacturers pivot between armored aerial lines and microcable runs with minimal downtime.

Smart machinery and PLC integration

Programmable logic controllers coordinate stranding frames, ribbon formers, and take-up units to keep tension within sub-0.01mm windows. Servo-driven extrusion coupled with laser micrometers enforce ±0.02mm jacket thickness. The result is fewer rejects, less rework, and consistent optical performance on every reel.

Edge processing and process coordination

Local edge servers ingest terabytes of telemetry each day. They drive low-latency closed-loop adjustments and push immediate alerts when deviations occur. This approach keeps optical fiber cable equipment running at peak efficiency. It supports real-time quality assurance during long production runs.

AGVs, material flow, and workflow gains

Automated Guided Vehicles move heavy cable drums with millimeter-level repeatability. Laser-navigated AGVs reduce manual handling injuries and speed material flow between extrusion, curing, and drum stations. This automation lowers labor costs while raising throughput on ftth cable production line technology setups.

Benefits for makers and the supply chain

  • Higher throughput with repeatable results
  • Quicker prototyping and a shorter path to market
  • Less labor risk and lower operational expense
  • Stronger connectivity between optical fiber cable equipment and enterprise platforms

Industry ecosystem and adoption

Leading telecommunications equipment manufacturers pair PLCs with robotic arms, AGVs, and industrial IoT stacks to reach Industry 4.0 goals. This integration creates a resilient production base. It is able to adapt as demand shifts toward denser, more complex FTTH offerings.

Precision Engineering Breakthroughs For Lower Attenuation

Advances in materials and mechanical design are driving down loss in modern fiber lines. Engineers pair ultra-low loss fiber with tighter coating control to reduce intrinsic and bending attenuation. These gains matter to network operators who want longer spans and fewer amplifiers in high-speed internet technology deployments.

The fiber optic cable production process now favors smaller coated diameters such as 180µm and 160µm. These sizes let manufacturers increase fiber count and build denser microcables without sacrificing handling or optical stability.

Low-Loss Glass And Advanced Coatings

Manufacturers use improved glass formulations that lower Rayleigh scattering and reduce baseline attenuation. Ultra-low loss fiber variants extend reach for long-haul and high-capacity links while easing repeaters and amplifier requirements.

Coating chemistry has progressed too. UV-cured acrylate systems cut microbending loss by roughly 40% compared with earlier generations. That performance drop helps maintain signal integrity in cramped ducts and tight bends common in FTTH and 5G backhaul networks.

Central Strength Members And Mechanical Design

Mechanical design updates center on robustness and dimensional control. Fiber-reinforced plastic (FRP) rods with tensile strengths near 1.2 GPa serve as central strength members. They limit elongation during pulling and boost crush and bending resilience.

Water-blocking advances use swellable yarns and grease-free gel compounds to achieve near-complete moisture resistance. These measures protect optical paths and raise in-service reliability for cable installations in challenging environments.

These precision engineering steps integrate directly into fiber optic cable manufacturing workflows. When the production line aligns glass, coating, and mechanical specs, attenuation falls and networks gain reliability. That alignment shortens time to service for operators deploying modern broadband and high-speed internet technology.

Quality Control 4.0 And AI-Powered Inspection

Smart factories for fiber optic cable production now embed inspection systems that run continuously. These systems combine machine vision, machine learning, and automated testers to watch every reel and spool. The result is tighter feedback during the fiber optic cable production process and fewer surprises in the field.

AI models score coating uniformity, microbends, and surface defects at line speed. They cross-reference process telemetry from fiber optic cable production machinery and predict deviations hours before a reel moves to final spooling. This allows for in-line adjustments without stopping the line.

Automated OTDR integration performs 100% attenuation testing on every length. Modern OTDR systems using 1550nm sources map loss across reels and flag changes as small as 0.01 dB/km. Inline OTDR logs feed edge analytics for rapid root-cause tracing when a batch shows anomalies.

Robotic bend-radius simulators apply repeated stress cycles while monitoring macrobend loss. These testers validate compliance with ITU-T G.657 and customer bend specifications by running controlled bends at multiples of the cable diameter. Test outcomes are tied to batch IDs for traceability.

Thermal cycling chambers stress jackets and splices across wide temperature ranges. Environmental tests up to +85°C and down to -60°C confirm stability for extreme climates. Automated logs record each chamber run and link results to production lots.

Quality control 4.0 reduces returns and field failures by making 100% in-line testing routine. Edge analytics and OTDR integration shorten diagnosis times and improve regulatory compliance. Broadband operators see fewer truck rolls and better lifecycle performance for FTTH networks.

Cable Design Innovations For FTTH Deployments

New cable designs address common field challenges in fiber to the home technology. Engineers focus on durability, space economy, and speed of activation. These trends reduce installation time and lower long-term operational costs.

Bend-Insensitive Fiber Benefits For MDUs And Tight Routing

Bend-insensitive fiber maintains signal strength when routed around corners and through confined spaces. ITU-T G.657 compliant fibers minimize attenuation at tight radii, protecting links in multi-dwelling units and behind baseboards. Prysmian’s BendBright family and BendBrightXS exemplify how smaller coated diameters facilitate routing without compromising optical performance.

Flat Drop And Microcable Options For Flexible Deployments

Flat drop cable remains a preferred choice for aerial self-support, duct installs, and direct burial in North America. Its profile accommodates narrow pathways and enhances aerial spans with appropriate clamps. High-fiber-count flat drops necessitate enhanced radial strength and more robust hardware for longer spans.

Microcable technologies reduce outside plant profiles to 8 mm or less. Microcables and air-blown systems enable capacity addition inside existing ducts and congested corridors. These approaches reduce civil works, lower labor costs, and facilitate incremental network growth for urban and campus builds.

Pre-Connectorized Solutions To Speed Field Activation

Pre-connectorized solutions offer factory-terminated, plug-and-play assemblies that minimize field fusion and connector errors. Hardened outdoor connectors and vendor offerings like Prysmian’s ezDROP simplify mass rollouts and enhance first-pass yield. Service teams experience fewer truck rolls and faster service turn-up for smart city and 5G edge projects.

Design Primary Benefit Common Use Case Deployment Consideration
Bend-insensitive optical fiber Stable performance in tight-radius routing Multi-dwelling units, indoor routing, compact pathways Select ITU-T G.657 variants for indoor runs
Flat drop Flexible installation options Aerial drops, direct burial, duct insertion Use correct clamps and hardware for radial strength
Microcable systems Compact profile with scalable capacity Microduct installations, crowded urban ducts Air-blown systems need compatible blower tools
Factory-connectorized solutions Quicker field activation with fewer errors Mass deployments, rapid service turn-up Standardized connector interfaces should be planned for

Sustainability And Energy Efficiency In Production Lines

Manufacturers in the fiber optic cable industry are embracing greener practices to reduce costs and meet consumer demands. Facilities prioritizing sustainable production witness improvements in operational efficiency and brand reputation. These advancements impact power systems, cooling, raw materials, and waste management.

Recovered energy systems strategies are becoming prevalent on extrusion lines and take-up reels. Regenerative braking on motor-driven spools returns power to the grid, thereby lowering net consumption. Studies indicate that energy recovery can reduce drive energy use by up to 32 percent in retrofitted reels.

Closed-loop cooling and chiller-less extrusion systems are reducing water demand. Adiabatic cooling can decrease water use by as much as 75 percent, particularly beneficial in water-scarce areas. Plants employing closed-loop cooling systems, in conjunction with heat exchangers, maintain temperature control while reducing utility expenses.

Recyclable jacket materials are transforming the disposal of cables. New polypropylene-based and modified polymer compounds meet mechanical and fire-safety standards, enabling higher recycling rates. Suppliers like Borealis and LyondellBasell are developing compounds that support the circular economy in cable jackets.

Process optimization minimizes scrap before recycling. Precision extrusion, in-line laser measurement, and real-time analytics reduce off-spec runs. Digital twins enable engineers to refine parameters, enhancing batch yields and reducing material waste.

Regulatory pressures and corporate ESG goals are compelling operators to favor vendors with transparent sustainability metrics. Municipal procurement teams and large network operators increasingly consider lifecycle impacts when selecting suppliers.

Focus Area Typical Improvement Primary Benefit
Regenerative drives on take-up reels Up to 32% energy reduction Reduced electricity costs and lower peak demand
Closed-loop cooling and adiabatic systems Roughly 75% less water use Lower water expenses and better compliance in arid areas
Recyclable jacket materials Higher post-consumer recycling rates Stronger circular economy support and easier disposal
Inline inspection and digital twins Double-digit cuts in scrap and off-spec runs Better yield, less material waste
Sustainability reporting and certifications Improved procurement positioning Competitive advantage with network operators

Implementing these measures enhances the resilience of fiber optic cable manufacturing. It leads to lower lifecycle costs and easier compliance. Manufacturers integrating energy recovery and recyclable jacket materials position themselves for growth in the green procurement market.

Emerging Technologies Shaping Cable Manufacturing

New technologies are transforming the design and operation of fiber optic cable production machinery. These innovations expedite commissioning, diminish prototyping cycles, and empower manufacturers to test process alterations without halting production.

Digital twins create virtual replicas of entire production lines and novel cable designs. Engineers at Corning and Prysmian leverage these models to validate footprint, material flow, and layout before physical construction. Studies indicate commissioning can be up to 60% swifter when teams execute virtual scenarios and optimize layouts beforehand.

Digital twins facilitate expedited R&D for bespoke items such as armored variants and anti-rodent jackets. Virtual testing minimizes the necessity for physical prototypes and accelerates market entry. Teams can simulate process modifications, observe material interactions, and refine equipment parameters in a risk-free milieu.

AI systems introduce predictive capabilities on the factory floor. Machine learning scrutinizes 50+ parameters to forecast failures and quality deviations hours in advance. This AI predictive maintenance lessens unplanned downtime and elevates overall equipment effectiveness for high-volume lines.

Manufacturers like Siemens and ABB integrate AI with edge computing, enabling models to operate proximal to machines. Alerts prompt targeted inspections, spare part staging, and corrective actions before a fault halts production. This strategy maintains yield and shortens mean time to repair.

Quantum fiber sensing and distributed monitoring extend capabilities beyond production to the deployed cable. Embedded Brillouin and distributed acoustic sensing provide continuous strain and temperature data across extensive spans.

Integration of quantum fiber sensing enhances network diagnostics and supports structural health monitoring. Field teams acquire actionable insights when sensing data is linked to manufacturing records and test logs. This connection enables tracing anomalies to specific production batches.

Combined workflows—digital twins plus AI predictive maintenance—accelerate both commissioning and product development. Manufacturers embracing these tools can respond more swiftly to market fluctuations and deliver higher-value, differentiated cables.

Market-Driven Production Adaptations And Regional Needs

The global demand for fiber access compels manufacturers to adapt their production lines to local requirements. Regional fiber optic cable manufacturing now emphasizes durability, density, and safety. Plants employ modular equipment, enabling swift transitions between product families and meeting specific operator needs without significant delays.

In North America, networks predominantly opt for aerial routes and robust outside-plant solutions. Producers concentrate on creating armored aerial cables with enhanced breaking strength, corrosion-resistant armor, and simplified pole-mount installation. These designs withstand wind, ice, and long span stresses typical of utility corridors.

North American Priorities: Aerial And Armored Designs

Armored aerial cables are engineered for enduring reliability on poles and open spans. They boast 1,200 lb or greater tensile ratings and integrated steel or aluminum armoring to safeguard fibers against mechanical damage. Manufacturers deploy modular armoring units and rapid testing rigs, enabling mass production of these variants.

APAC And Europe: High-Density Microcables And Regulatory Compliance

In APAC, the scarcity of space and the need for dense builds drive demand for high-density microcables. These cables feature compact stranding towers and reduced-diameter fiber stacks, allowing for more fibers per duct. They significantly reduce civil costs by facilitating quicker overbuilds and easier microtrenching.

Europe mandates strict regulatory compliance for buildings and public spaces. Producers offer halogen-free, flame-retardant jackets that meet CPR classes like B2ca. Compliance testing is integrated into production lines, ensuring products meet fire-safety rules for indoor and outdoor applications promptly.

Across regions, the ability to adapt production is paramount. Compact stranding towers, modular extrusion and armoring units, and rapid prototyping enable factories to switch from armored aerial cables to microcable runs in mere hours. This flexibility allows operators to fulfill unique specifications while adhering to local codes.

Case Studies And Manufacturer Spotlight: Shanghai Weiye OFC Equipment

Shanghai Weiye OFC Equipment has solidified its reputation as a leading telecommunications equipment manufacturer. They cater to the FTTH and broader fiber markets. Their optical fiber cable equipment boasts advanced features, including SZ stranding, ribbon production, and extrusion with servo control. This ensures tight tolerances and high yields.

Their machinery for fiber optic cable production is equally impressive. It includes tape armoring units, automated take-up reels with regenerative drives, and integrated OTDR and vision inspection stations. These systems support various applications, such as bend-insensitive fiber, microcables, and pre-connectorized solutions. These are crucial for FTTH, 5G backhaul, and dense urban deployments.

Quality and sustainability are integral to their offerings. They employ OTDR testing, AI-powered inspection, and robotic bend simulators to meet QC 4.0 standards. Additionally, energy recovery options and closed-loop cooling reduce operating costs and scrap. Modular designs with AGV and edge computing support enable rapid reconfiguration and digital twin commissioning, catering to U.S. manufacturers and contract producers.

For operators in the United States, investing in Shanghai Weiye OFC Equipment can significantly enhance production capabilities. It ensures compliance with strict attenuation and mechanical specifications. This accelerates the introduction of new cable families, vital for broadband expansion. The company’s systems harmonize technical performance with practical manufacturing requirements.

FAQ

Q: What Advances Define Modern FTTH Cable Production Line Technology?

A: Modern FTTH cable production lines integrate high-precision mechanical systems with servo-driven extrusion. They utilize SZ stranding and ribbon machines, along with automated take-up reels. These systems also include integrated OTDR and AI-driven vision inspection, PLC orchestration, AGV material handling, and edge computing. Such advancements enable micron-level tension control and ±0.02mm jacket thickness tolerances. They achieve 95%+ automation and 100% in-line testing, reducing attenuation, scrap, and time-to-market.

Q: How Do You Define The Scope Of FTTH Cable Production Line Technology?

A: FTTH cable production line technology includes the machinery, process controls, and materials for fiber-to-the-home networks. It includes optical fiber drawing and coating, SZ stranding, and ribbon formation. Extrusion of inner and outer jackets, armoring or taping modules, and automated take-up and drum handling are also part of it. In-line optical and mechanical testing, along with the software stack—PLCs, edge servers, and industrial IoT—are integral to the process.

Q: Why Does Production-Line Quality Matter For Broadband Network Infrastructure?

A: Production-line quality directly impacts attenuation, splice loss, mechanical robustness, and long-term reliability. High-precision manufacturing minimizes intrinsic and macrobending losses. It extends reach, lowers field interventions, and improves first-pass yields. For carriers and ISPs, this translates to fewer truck rolls, lower total cost of ownership, and higher service availability for high-speed internet, 5G backhaul, and symmetrical multi-gigabit home services.

Q: What Role Do PLCs And Smart Machinery Play In Industry 4.0 Production Lines?

A: Programmable logic controllers (PLCs) provide deterministic synchronization across SZ stranding, ribbon forming, and take-up units. They enable sub-0.01mm tension precision, closed-loop extrusion control, automated recipe changes, and safety interlocks. When combined with robotic arms and automated armoring modules, PLCs form the backbone of Industry 4.0 production. They drive repeatability and high throughput with minimal human intervention.

Q: How Are AGVs And Edge Computing Used On Modern Cable Production Floors?

A: Laser-navigated AGVs move heavy drums and material spools with high positioning accuracy. Industry examples show 1,200kg capacity and sub-5cm placement. Edge computing processes terabytes of telemetry locally, delivering low-latency analytics and real-time quality alerts. Together, AGVs and edge computing improve material flow, reduce manual handling risks, and enable rapid correction of process deviations.

Q: What Precision Engineering Improvements Reduce Optical Attenuation?

A: Improvements include ultra-low-loss (ULL) glass formulations and advanced UV-cured acrylate coatings. These coatings cut microbending losses. Smaller coated diameters (e.g., 160–180µm) enable denser cable designs. Tight control of drawing tension, coating cure profiles, and extrusion concentricity—monitored by laser micrometers and closed-loop controls—lowers intrinsic loss and fluctuation across production reels.

Q: How Do Central Strength Members And Mechanical Design Affect Cable Performance?

A: Mechanical designs incorporating fiber-reinforced plastic (FRP) rods or high-strength central members control elongation during installation. They resist crush and bending, protecting fiber glass from strain. Proper selection of strength elements and buffer constructions reduces installation-induced loss, improves long-term reliability, and supports aerial or duct deployments with demanding mechanical requirements.

Q: What Does “QC 4.0” Mean And How Is It Implemented?

A: QC 4.0 describes a fully instrumented, data-driven quality-control regime. It includes 100% in-line testing, AI-powered vision inspection, automated OTDR mapping, robotic bend tests, and environmental chambers integrated into the production workflow. Edge analytics, traceable test logs, and predictive models enable rapid root-cause analysis, minimize returns, and ensure compliance with ITU-T and operator specifications.

Q: How Is OTDR Testing Integrated Into Production And What Sensitivity Can It Achieve?

A: Automated OTDR stations are integrated inline or at take-up to perform full-length attenuation mapping. They use dual-wavelength sources (including 1550nm). Modern setups can detect variations down to 0.01 dB/km, map localized defects, and tie results to batch IDs for traceability. This enables manufacturers to flag and quarantine reels before shipment, improving field reliability.

Q: What Are Robotic Bend-Radius Simulators And Thermal Cycling Chambers Used For?

A: Robotic bend-radius simulators apply repeated controlled bends and record macrobend loss to verify compliance with ITU-T G.657 and customer specs. Thermal cycling chambers run jackets and assemblies through −60°C to +85°C cycles to validate dimensional stability, jacket adhesion, and splice performance under extremes. Automated test logs provide traceable evidence for operator and regulatory requirements.

Q: What Cable Design Innovations Are Most Relevant To FTTH Deployments?

A: Key innovations include bend-insensitive fiber (BIF) for tight routing in MDUs and indoor paths. Flat drop and high-fiber-count flat assemblies are used for aerial and direct-burial North American use cases. Microcables and air-blown systems are for duct-constrained environments. Pre-connectorized assemblies speed field activation and reduce termination errors.

Q: Why Is Bend-Insensitive Fiber Important For MDUs And Tight Routing?

A: Bend-insensitive fiber maintains low loss under tight radii and repeated handling. It is crucial in multi-dwelling units, plenum runs, and behind baseboards. ITU-T G.657-compliant fibers help prevent macrobending loss during installation and reduce service calls related to routing-induced degradation. They support denser routing with fewer installation constraints.

Q: How Do Flat Drop Cables And Microcables Differ In Deployment Benefits?

A: Flat drop cables offer flexible aerial and direct-burial deployment with compact profiles suited to service drops. Microcables (≤8mm) and microduct systems excel in congested ducts and enable incremental capacity growth via air-blown installation. Choice depends on regional deployment practice, span requirements, and operator preferences.

Q: What Advantages Do Pre-Connectorized Solutions Provide?

A: Factory-terminated, hardened pre-connectorized assemblies reduce field splicing, eliminate human termination variability, and speed up service activation. They improve first-pass yield. Products like hardened OptiTap-style connectors and vendor pre-terminated drops support rapid mass-deployment strategies and lower workforce training needs.

Q: How Are Energy Recovery And Cooling Innovations Improving Sustainability?

A: Regenerative drives on take-up reels and motor assemblies can capture braking energy, reducing net consumption by industry-reported amounts (example: up to ~32%). Chiller-less or adiabatic extrusion cooling reduces water use by up to 75%. These measures lower operational cost, reduce water consumption, and align production with corporate sustainability targets.

Q: Are Recyclable Jacket Materials And Waste Reduction Practical For Production?

A: Yes. Recyclable compounds such as specially formulated polypropylene-based jackets can meet mechanical and flame performance while improving end-of-life recycling. Precision extrusion and in-line inspection reduce scrap rates. Combined with material-efficient tooling and digital-twin optimization, manufacturers can materially lower waste and support circular-economy goals.

Q: What Role Do Digital Twins Play In Cable Manufacturing?

A: Digital twins create virtual replicas of production lines and cable designs to simulate process changes and validate material flow. They accelerate commissioning. Industry estimates show commissioning and prototyping time reduced significantly (case examples up to ~60%). Digital twins also support offline testing of recipe changes and faster roll-out of new product families.

Q: How Does AI Enable Predictive Maintenance And Quality Prediction?

A: Machine learning models trained on dozens of production parameters can forecast equipment faults hours in advance and predict quality drift. Predictive maintenance reduces unplanned downtime, improves OEE, and allows planned service windows. AI-driven quality models provide early alerts for deviations that would otherwise produce rejects or field failures.

Q: What Is The Significance Of Quantum And Distributed Sensing Integration In Cables?

A: Embedding distributed sensing capabilities—such as Brillouin-based strain sensing and distributed acoustic sensing (DAS)—adds network-level telemetry for structural health monitoring, intrusion detection, and environmental diagnostics. Integrating sensing into cable designs enables added-value services and improved operational visibility for carriers and critical infrastructure owners.

Q: How Do Production Lines Adapt To Regional Market Needs (North America, APAC, Europe)?

A: Lines are modular and reconfigurable to meet regional priorities. North America focuses on robust aerial and armored designs with higher breaking-strength requirements for pole deployments. APAC emphasizes high-density microcables and compact stranding for dense urban rollouts. Europe prioritizes halogen-free flame-retardant jackets and CPR fire-class compliance. Modular stranding towers, quick-change extrusion heads, and configurable armoring units enable fast changeovers.

Q: What Manufacturing Equipment Is Essential To Support Varied FTTH Product Families?

A: Essential equipment includes SZ stranding machines (dozens to hundreds of fibers with micron-level tension control), ribbonization lines, servo-driven extruders with laser micrometers, tape or armor-wrapping stations, automated take-up reels with regenerative drives, inline OTDR and AI vision inspection, AGV drum handling, and edge computing/PLC orchestration for Industry 4.0 integration.

Q: How Do Manufacturers Ensure Compliance With Standards Like ITU-T G.657 And Regional Safety Codes?

A: Compliance is ensured via precise material selection (bend-insensitive fiber types), controlled production recipes, automated in-line tests (OTDR, macrobend testers), and environmental qualification (thermal cycling, flame tests). Traceable test logs, batch IDs, and documented QC protocols align production outputs with ITU-T recommendations and regional regulations such as CPR classifications in Europe.

Q: What Benefits Can U.S. Manufacturers Expect From Equipment Suppliers Like Shanghai Weiye OFC Equipment?

A: Suppliers like Shanghai Weiye provide modular, Industry 4.0-ready production machinery—SZ stranding, ribbon lines, precision extrusion with closed-loop controls, AI inspection modules, and integrated OTDR testing. This enables U.S. contract manufacturers and in-house producers to scale FTTH output, maintain tight attenuation and mechanical tolerances, adopt sustainability options (energy recovery, closed-loop cooling), and shorten time-to-market for variants such as armored aerial, flat drop, microcable, and pre-connectorized assemblies.

Q: How Do In-Line AI Inspection Systems Detect Subtle Defects At Production Speed?

A: AI-powered machine vision inspects coating uniformity, surface defects, and microbends using high-resolution cameras and convolutional models trained on labeled defect libraries. Models correlate dozens of parameters—diameter variance, coating texture, micro-crack signatures—to predict deviations hours before they become out-of-spec reels. This enables automated rejection, parameter adjustment, and reduced downstream field failures.

Q: What Testing Sensitivity And Traceability Are Achievable For Attenuation And Mechanical Validation?

A: Modern production lines integrate automated OTDR systems capable of resolving 0.01 dB/km changes, robotic bend simulators for repeated macrobend stress testing, and thermal chambers for extreme environment validation. Test results are stored with batch and reel identifiers in edge or cloud databases, providing full traceability for operator acceptance, regulatory audits, and customer service diagnostics.

Q: How Do Production Innovations Translate Into Market Outcomes For Network Operators?

A: Innovations in manufacturing yield lower-loss fibers, denser cable designs, and factory-terminated assemblies that reduce installation time and errors. Operators benefit from higher service reliability, fewer truck rolls, lower lifecycle costs, and faster rollout of symmetrical multi-gigabit services. These outcomes support widespread FTTH adoption, 5G backhaul capacity, and scalable connectivity for smart cities and hyperscale data center interconnects.

Related: Compact Fiber Unit Process Control for Stable Dimensions
Why Quality Control Matters in a CNC Machine Shop in Houston

Were you aware that precision components support over 30% of Houston’s industrial output? This reliance on exacting standards creates a constant need for expert fabrication.

Visit Website of Industrial Machining Services in Houston
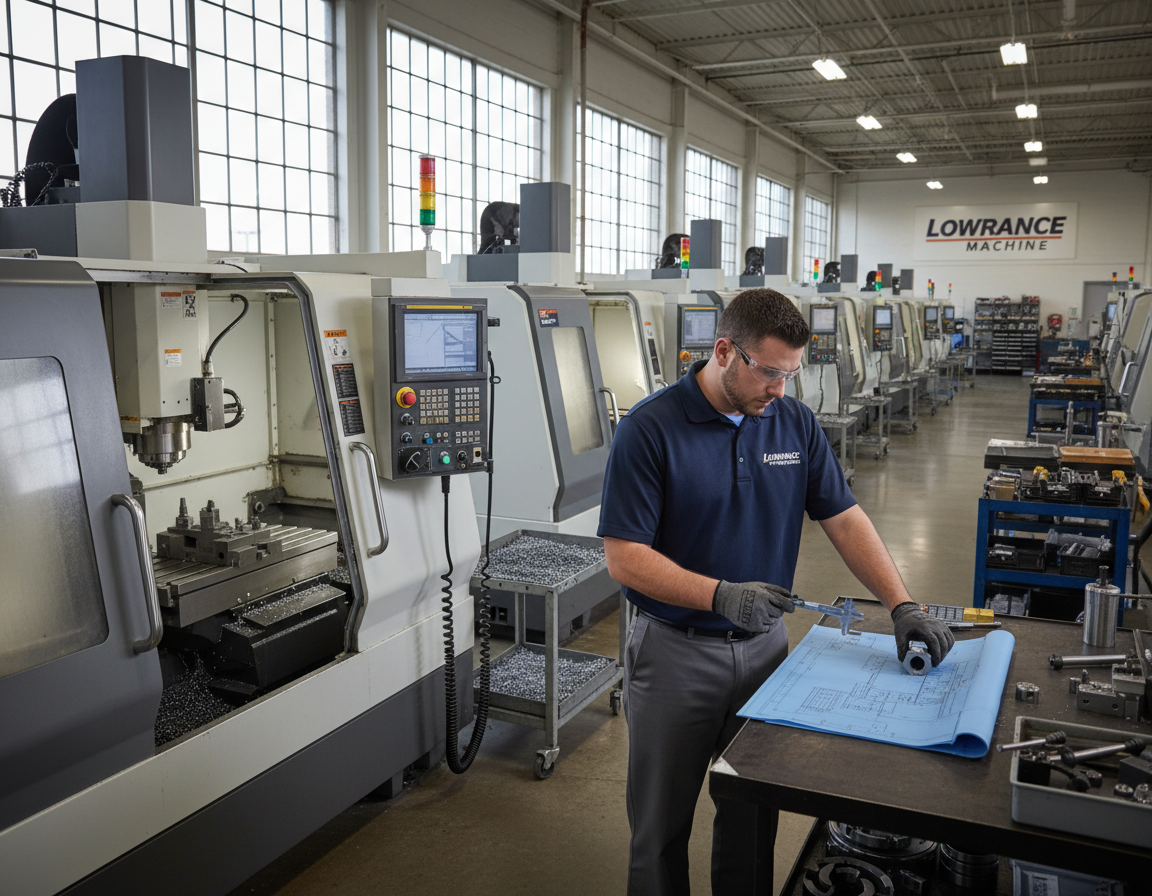
Lowrance Machine meets this demand as the area’s premier CNC machine shop. We provide advanced machining solutions for a wide range of industries.

Our commitment to quality is unwavering. Every part we produce undergoes rigorous checks for accuracy and reliability.

The facility houses state-of-the-art, computer-controlled equipment. This technology allows for superior results and complex geometries.

Clients trust us as a partner for critical projects. Our professional service and technical expertise ensure expectations are not just met, but exceeded.

We are the go-to source for precision-machined components. Our machining expertise covers everything from prototype to production runs.

The following sections detail our comprehensive capabilities.

Welcome To Lowrance Machine: Precision CNC Machining Experts

In a world where margins are measured in thousandths of an inch, only the most dedicated teams succeed. We are proud to be your local partner for exceptional fabrication.

Our core mission is delivering unwavering quality standards with every part we create.

Our Commitment To Quality And Reliability

For decades, shops in this region have built their names on consistent results. We continue that legacy. Every project undergoes rigorous checks from design to delivery.

Our skilled team brings deep technical knowledge to ensure superior outcomes. This focus on precision minimizes risks for your project.

True quality is never accidental; it is always achieved through intelligent effort.

The table below highlights key aspects of our professional approach.

Industrial Machining Services in Houston

Service Focus Our Benchmark Client Benefit
Quality Control Layered inspection process Improved consistency and reduced waste
Team Expertise Extensive combined experience Precise and complex components
Service Range Local service plus national delivery Dependable supply continuity

Serving Houston And Beyond

We build lasting partnerships based on trust and consistency. Our machining services extend across Texas and nationwide.

You can count on us for clear communication and on-time delivery. We understand that your success depends on a stable, dependable partner.

Let’s discuss how our experience can bring your project to life.

Our Comprehensive CNC Machining Capabilities

From intricate prototypes to robust production runs, success hinges on a broad set of machining skills. Our facility delivers a full suite of fabrication services to meet any challenge.

Milling, Turning, And Drilling Services

Our cnc milling capabilities produce parts with complex geometries and excellent surface finishes. Advanced lathes handle precise cnc turning for cylindrical components.

We also perform standard and deep-hole drilling. This includes gun drilling for holes up to 116 inches long.

Specialized Techniques For Complex Parts

Live tooling combines turning and milling operations for efficiency. We also use wire and probe EDM to create virtually any part geometry.

This variety of techniques lets us tackle components others might find impossible. We handle a wide range of sizes and complexities.

CNC Machine Shop In Houston: Precision Services Tailored To Your Needs

The true mark of a skilled fabricator lies in adapting processes to fit exact requirements. We specialize in cnc machining services that are customized for your unique situation.

Our process begins with a conversation. We listen to understand your specific needs and the goals of your project.

This consultative approach ensures the final precision machined parts function perfectly. We also offer design assistance to optimize your concept for manufacturing.

Customer Need Our Response Key Result
Custom Specifications Custom CNC programming Exact Fit & Form
Complex Component Shapes Advanced Multi-Axis Machining Consistent functional results
Changing production volume Adaptable process planning Uniform quality at every volume

We handle everything from one-off prototypes to full production runs. Every batch of machined parts delivers the same precision machined excellence.

Our collaborative process means engineers work alongside you. The goal is to achieve outcomes that surpass expectations for every component.

State-Of-The-Art Technology And Equipment

Staying ahead in modern manufacturing requires a constant commitment to technological advancement. We have made significant investments in the latest cnc machine technology to empower our team.

This ensures we deliver the precision and reliability our clients depend on for critical applications.

Advanced Mori Seiki CNC Machines

Our recent acquisitions include advanced Mori Seiki and DMG MORI models. The fleet features two NLVX7000 4-axis mills with rotary tables and a new DMG MORI NVX 7000.

We also utilize a CMX100 4-axis mill and an NLX3000 with Live Tooling. These machines form the core of our enhanced machining capabilities.

Equipment Model Key Feature Primary Advantage
DMG MORI NLVX7000 / NVX 7000 4-axis milling with rotary table High-speed cutting and complex geometry
CMX100 4-Axis Vertical Machining Center Superior surface finish & rigidity
NLX3000 with Live Tooling Multi-Tasking Turning Center Reduced setups and greater efficiency

Enhanced Capabilities In Aerospace And Medical Machining

This advanced equipment is crucial for aerospace and medical sectors. These industries demand extreme accuracy and flawless surface integrity.

Our climate-controlled facility ensures optimal conditions for consistent, quality results. We work with a vast range of materials, from stainless steels to specialized alloys.

Combining cutting-edge cnc technology with highly skilled machinists guarantees superior outcomes for every project.

Extensive Industry Experience And Versatile Applications

From the skies to the sea floor, precision components are the unsung heroes powering modern industry. Our team has built deep experience serving a wide variety of critical sectors.

Solutions For Aerospace, Energy, And Military Sectors

We provide specialized machining for the aerospace industry. This includes work for NASA and other firms in the area requiring ultra-precise parts.

The energy sector relies on our reliable components for demanding applications. We serve major oil and gas companies with high-quality, durable pieces.

Military projects demand strict adherence to specifications and security. Our work also extends to biomedical, marine, and automation industries.

Prototyping To Full-Scale Production

We guide products from initial concept through final production. This full lifecycle support is invaluable for development.

Our capabilities cover everything from a single prototype to a large production run of thousands. We handle this wide range of volumes with consistent quality.

This broad variety of industries enriches our problem-solving toolkit. Best practices from aerospace machining benefit all our clients.

Quality Assurance, Safety, And Competitive Pricing

Value in precision fabrication isn’t just about price. It’s about consistent performance over time.

We achieve this through a dual commitment to rigorous checks and streamlined operations.

Rigorous Quality Control Processes

Our system is built on ISO 9000 principles. We employ Statistical Process Controls to maintain tight tolerances.

This minimizes scrap and waste while ensuring every part meets exact specifications.

That confidence is backed by our satisfaction guarantee. We correct issues if expectations are not completely fulfilled.

This focus on quality CNC machining yields durable, reliable components. They perform consistently in the most demanding applications.

Cost-Effective Production Without Compromise

Our competitive pricing structure provides exceptional value. It never sacrifices accuracy or quality.

Built-in production and process efficiencies save clients money. A focus on productivity reduces time and prevents material waste.

Treating customers right begins with respecting their budgets. You receive superior precision parts today and every day.

Integrated Services And Personalized Customer Support

A truly efficient manufacturing partner does more than just cut metal. They provide a complete solution from start to finish.

This integrated approach saves you time and simplifies logistics. You have a single, accountable source for your entire project.

One-Stop Shop For Metal Fabrication And Finishing

Our comprehensive fabrication services include vital finishing steps. We perform heat treating, powder coating, plating, and anodizing in-house.

Additional treatments like passivation and laser etching are also available. TIG, MIG, and ARC welding complete our metal fabrication capabilities.

Our square foot facility is designed for flexibility. It supports both short-run prototypes and high-volume production.

Customer Challenge Our Complete Solution Primary Advantage
Coordinating Multiple Vendors Fully in-house fabrication and finishing Simplified Management & Single Point of Contact
Special finishing requirements Multiple finishing services under one roof Enhanced Durability & Performance
Changing order volume Adaptable production planning and floor capacity Consistent Quality for Any Order Size

Timely Project Delivery And On-Demand Support

We operate extended hours to meet tight deadlines. Our team provides same-day quotes and is ready to assist with your design questions.

Warehousing and just-in-time delivery options ensure a steady flow of parts. This is ideal for clients across the Houston area and beyond.

You can rely on us for responsive support and reliable timelines. We become a true extension of your operation.

Conclusion

Your search for a reliable source of premium machined parts ends here. Lowrance Machine is the region’s leading fabrication partner, delivering unmatched precision and a full spectrum of machining services.

Our skilled team utilizes advanced technology in a spacious facility to achieve superior outcomes. We work with a wide range of materials and serve diverse industries, from single prototypes to large production volumes.

Expanded shop hours and a satisfaction guarantee ensure fast, reliable delivery. Whether you need design support or a quick quote, our experts have the capabilities to make your project a success.

Get in touch today to partner with a trusted leader in precision fabrication.

Related: Mold Design Houston – Your One-Stop Shop for Complete Tooling

The Legacy of WWII Innovation on Modern CNC Precision Machining

KZD-CncMmachining.com specializes in providing CNC Precision Machining know-how for a wide range of industry sectors such as aerospace, medical, energy, and automotive. It uniquely combines high-end machining technology alongside a team of experienced engineers. Their mission is to turn complex designs into real-world parts. Top-tier operations such as RAM Tool and WessDel represent top performance through broad capabilities, adherence to ISO-certified quality measures, and a diverse array of machinery capable of managing substantial workpieces and demanding precision.

Advanced CNC precision machining significantly decreases production cycles, cuts material waste, while boosting part-to-part consistency. This happens through a synergy of CAD/CAM programming workflows, modern machining centers, and rigorous quality controls. A dependable CNC machine shop offers customizable CNC machining and contract manufacturing services. It smoothly scales from initial prototype stages to comprehensive production volumes, prioritizing meticulous inspection and end-to-end traceability at every step.

At KZD-CncMmachining.com, our strength is a client-focused approach, comprehensive metrology analysis, and the provision of end-to-end solutions. Our experience serves single-run CNC machining projects and the mass production of high-volume components. Through an optimal combination of advanced machinery plus disciplined process control, we guarantee consistent, precise results.

Key Takeaways

  • KZD-CncMmachining.com is dedicated to CNC precision machining for many industries.
  • Advanced machines such as 5-axis platforms and horizontal mills expands capability for complex parts.
  • CNC precision machining cuts mistakes and improves repeatability through CAD/CAM and inspection.
  • Custom CNC machining and scalable CNC machining services cover prototype work through production runs.
  • Quality systems and metrology are critical to meet tight tolerances and industry standards.

CNC Precision Machining Solutions

Digital designs morph into precise parts for aerospace, medical, and industrial applications through CNC precision machining. Experts at facilities like RAM Tool and Precision Automation rely on CAD/CAM files for machine setup. They engage mills, lathes, and CNC routers to produce dies, prototype tooling, and custom components. Thorough inspections and punctual deliveries remain central to this workflow.

CNC Precision Machining

Definition And Core Benefits Of CNC Precision Machining

CNC production propels cutting tools via computer numerical control, ensuring exceptional accuracy. It remarkably diminishes manual setup, reduces cycle times, and limits errors. Capabilities include milling, turning, true 5-axis machining, and wire EDM, handling detailed geometries and strict tolerances with efficiency.

Typical Tolerances And Material Capabilities

Precision machining often achieves tolerances as tight as 0.0002″ on steel and titanium alloys such as Ti-6Al-4V. Typical stainless grades machined include 15-5, 17-4, 304, 316, and 420. The material mix extends from aluminum and zinc for die casting to robust steels, titanium, and engineered plastics for a range of industrial needs.

How Precision CNC Machining Reduces Error And Improves Repeatability

CAM programming with deep tool libraries and automated probing curtail variation, improving consistency. Metrological instruments, including CMMs and laser scanners strengthen part-to-part accuracy. This improved efficiency speeds the progression from prototypes to full-scale production while maintaining strict quality control with traceable records.

Comprehensive CNC Machining Services For Custom Components

Producers require complete capabilities for fast turnaround on precision components. Modern CNC shops blend CNC milling and CNC turning with specialized processes. This enables prototypes, short runs, and full production volumes. Operations including RAM Tool, WessDel, and Precision Automation facilities illustrate integrated workflows. These enhance design, inspection, and logistics processes for customized CNC machining programs.

CNC milling services support intricate shapes and prototype builds by using multi-axis mills and broad CAM libraries. Shops handle tooling for aluminum die casting and detailed features including pockets and ribs. Methods such as laser scanning and reverse engineering workflows enhance inspection data. This accelerates changes and helps ensure schedules are met.

CNC turning services focus on cylindrical parts and large-scale shaft production. The arrangement of lathe-based cells help maintain uniformity and consistent finishes. Merging turning and live tooling allows for the creation of complex parts in a single sequence. This method reduces processing time while minimizing costs for large production programs.

EDM and wire EDM processes provide solutions for intricate designs in difficult-to-machine materials. These technologies craft thin slots, sharp internal angles, and refined profiles beyond the reach of milling. Supporting steps such as heat treatment, deburring, and finishing help deliver parts that are ready to install.

Capability Common Use Customer Value
Multi-axis CNC milling capability Prototype work, complex contours, die tooling Reduces setups, improves accuracy, supports tight tolerances
CNC turning with live tooling capability Shafts, bushings, threaded components Speeds production, combines operations, cuts lead time
Wire EDM and EDM Hard materials, thin features, and mold components Enables intricate shapes, maintains fine detail, preserves hardness
Laser scanning & metrology Reverse engineering, inspection, quality control Validates parts, supports custom CNC machining revisions, ensures compliance
Heat treating and finishing Material strengthening, corrosion resistance, final finish Delivers turnkey parts ready for assembly or end use

Selecting the right CNC machine shop means aligning machinery with your part specs. Seek facilities that amalgamate CNC milling, CNC turning, and EDM with inspection and assembly capabilities. This synergy controls lead times effectively. It ensures delivered parts match engineering intent.

Advanced Machining Technologies And Equipment In CNC Shops

High-performing facilities implement a synergistic array, featuring multi-axis platforms, fast machining centers, and robust equipment for demanding designs and tight tolerances. Reliance on trusted brands like Hermle, DMG Mori, OKK, and Mitsubishi machines, reflects dedication to higher productivity and consistent results through precision machining operations.

5-Axis And Multi-Axis Machining For Complex Components

5-axis centers help engineers consolidate operations previously done across many setups. Using true 5-axis machining speeds completion of parts with deep cavities, angled features, or complex shapes. This reduces manual intervention, abbreviates the production cycle, and preserves geometric accuracy, particularly for aerospace and medical devices.

High-Speed Machining Centers And Horizontal Boring Mills Equipment

The adoption of high-speed milling techniques results in better surface finishes and diminished lead times for softer materials and composites. On the other hand, horizontal boring mills increase tool efficiency and minimize detrimental chip interference on substantial segments. Strategically combining high-speed and horizontal equipment improves shop versatility to take on both small intricate pieces and large structural components.

Coordinate Measuring Machines (CMM) And Metrology For Quality Assurance

A well-rounded metrology approach brings together CMM probing, laser checks, and digital summaries to compare accurately against CAD models. These advanced systems support strict AS9100 and ISO 9001 requirements. By correlating measurement outcomes with procedural adjustments, a leading CNC shop limits deviation while substantiating adherence to regulatory demands.

The integration of avant-garde machinery with a solid quality framework reduces scrap and rejections while accelerating the shift to full production. A balanced mix of technology and precision measurement affords scalable solutions, from prototypes through full-scale production.

Industry Applications And Material Expertise

Advanced machining is vital for manufacturers to satisfy strict requirements of various sectors. Operations like RAM Tool, WessDel, and Precision Automation facilities highlight the importance of specialized processes and deep material knowledge for performance optimization. They cater to industries including aerospace, medical, energy, automotive, mining, and heavy industrial equipment manufacturing.

Aerospace And Defense: Lightweight Alloys And Strict Standards

Aircraft and defense components necessitate rigorous control over aspects like weight, strength, and endurance. Aluminum alloys and Ti-6Al-4V are frequently machined for airframes, engines, and structural parts. Precision CNC machining adheres to tight tolerances and upholds AS9100 standards for comprehensive traceability.

Companies such as RAM Tool and WessDel facilities deliver parts built for extreme conditions. They implement processes such as surface finishing and heat treatment, key for flight and defense applications. Their custom CNC machining supports production of small flight hardware plus varied precision parts.

Medical And Life Sciences: Tight Tolerances And Traceability

Producing medical device components requires achieving micrometer-level tolerances while preserving rigorous traceability. Using clean-room practices and strong lot control is crucial to meeting both FDA and ISO 13485 standards. Through precision CNC machining, manufacturers can create complex geometries for implants, surgical tools, and diagnostic devices.

Material choices include stainless steel, cobalt-chrome, and titanium alloys. WessDel and other specialized shops underscore the importance of documentation and serialization. This level of detail ensures regulatory compliance and supply-chain integrity, enabling prototype work and regulated production runs.

Energy, Automotive, Mining, And Industrial Equipment Applications

Within energy and heavy-industry sectors, the demand for durable parts from hardened steels and specialty alloys is critical. Equipment like horizontal boring mills is vital for machining large components. This CNC approach merges efficient material removal with temperature management, producing consistent results.

Automotive and powersports manufacturers demand quick production times and consistent quality. Through precision CNC machining, they minimize waste and enhance production efficiency. Precision Automation, for example, keeps machining in-house. This supports OEM assembly lines and the build of robotic subassemblies.

The table below summarizes key differences across industries, typical material choices, and the machining priorities that influence sourcing decisions.

Sector Typical Materials Primary Machining Priorities
Aerospace & Defense Aluminum alloys, Ti-6Al-4V titanium, nickel alloys Tight tolerances, traceability, surface finish, certification
Medical & Life Sciences Stainless steel (316L), cobalt-chrome, titanium Micron tolerances, lot control, clean-room processing
Energy & Power Heat-treated steels, Inconel, specialty alloys Large-format machining, heat-treat compatibility, wear resistance
Automotive & Powersports Steel, aluminum, case-hardened alloys Repeatability at volume, cycle-time optimization, cost control
Mining & Industrial Equipment Forged steels, wear-resistant alloys Durability, heavy-duty fabrication, large-capacity machining

Selecting suppliers experienced with these materials lowers risk. Companies that merge profound material knowledge with verified CNC manufacturing techniques deliver more predictable, cost-efficient paths from idea to production. This integration elevates the predictability and cost-effectiveness of custom CNC machining projects.

Quality Systems, Tolerances, And Inspection Processes

Design intent transforms into reliable components via robust quality systems and strict inspection protocols. CNC machining services integrate ISO/industry standards with manual checks. This ensures compliance to aerospace, medical, and industrial specifications. Production remains consistent, ensured by clear traceability and meticulous documentation from initial production to full-scale operations.

Systems such as ISO 9001 and AS9100 provide ongoing control and audit readiness. WessDel adheres to these standards, ensuring parts meet strict criteria. Precision Automation employs ISO 9001 methodologies alongside CAD/CAM processes. This ensures machinists produce components passing strict inspections.

Inspection methods differ across facilities yet utilize common instruments: CMMs for dimensional verification, laser scanners for complex geometry, plus dedicated gauges to verify fit and function. RAM Tool possesses a dedicated CMM inspection division, enhancing it with laser scanning for reverse engineering and superior quality assurance. These tools are critical for verifying key attributes.

A common inspection flow starts with a CAD-driven tolerance evaluation, then first-article inspection and CMM validation. Laser scanning is employed to verify complex surfaces and assist reverse engineering. Comprehensive documentation, including serial numbers, operator approvals, and measurement data, guarantees traceability.

Tolerance capability depends by the chosen material and method. For stainless steel and titanium work, entities like RAM Tool achieve tolerances as strict as 0.0002 inch for particular parts. This precision emphasizes the importance of meticulous setups, dependable tooling, and skilled personnel inside a dedicated CNC manufacturing operation.

Selecting a partner with precise metrology tools, defined procedures, and capable technicians is critical to achieve high-quality CNC machining outcomes. A well-run CNC machine shop builds thorough inspection into production, ensuring parts leave with confirmed compliance and reliable performance.

From Prototype To Production: Contract Manufacturing And Turnkey Solutions

Transitioning a concept into a tangible item entails a blend of expertise in prototype tooling, swift modifications, and extensive machining. Organizations such as RAM Tool and WessDel show how laser scanning and reverse engineering speed prototype development. Precision Automation demonstrates integrated in-house machining plus assembly lines for delivering complete systems, while adhering to ISO 9001 standards.

Prototype tooling & reverse engineering

Initiating with rapid production of fixtures and selective enhancements of heat treatment or surface qualities, prototype tooling sets the foundation. Through laser scanning, teams capture existing-part dimensions for reverse engineering, avoiding lengthy CAD redesigns. This technique notably shortens iteration time, improving fit and maintaining part quality.

Scalable contract manufacturing services

Contract manufacturing covers the range from low-volume lots for validation to high-volume production for launch. At both levels, custom CNC machining transitions from single-item operations to automated cell layouts. When production scales up, CNC machining services adeptly adjust programming, tooling setups, and inspection processes.

Subassembly, wiring & machine rebuilding

Full turnkey solutions commonly include subassembly, automated control-panel wiring, and full machine refurbishment. Subassembly services reduce the assembly load on the customer. Refurbishing and updating equipment not only prolongs their operational lifespan but also conserves financial resources and helps maintain reliable uptime.

Capability Typical Offerings Value to Customers
Prototype Tooling Rapid fixtures, soft jigs, small-batch molds Faster design validation, lower upfront cost
Reverse Engineering Laser scanning, CAD recreation, fit checks Recreate legacy components, cut redesign time
Custom CNC Machining Services 5-axis milling, turning, precision finishing operations Accurate, repeatable production
Contract manufacturing Low- to high-volume runs, kitting, logistics Scale without capital expansion
Subassembly & Wiring Automated panel wiring, functional test Plug-and-play delivery, reduced assembly workload
Machine rebuilding Refurbish spindles, retrofit controls Extended equipment life, better performance

Opting for a collaborative partner with vast capabilities in CNC manufacturing minimizes transitions and expedites timelines. Bringing DFM insight and complete CNC machining services under one contract manufacturing arrangement clarifies responsibility. This supports quicker market entry for new products.

Choosing A CNC Machine Shop: What To Look For In A CNC Partner

Choosing the right partner for precision work is essential. A high-performing CNC shop brings together strong technical skill, modern equipment, and dependable service. Prioritize finding a partner with documented quality systems, clear capacity and capability visibility, plus demonstrable experience in your sector.

Technical Expertise, Skilled Machinists, And Engineering Support

Ensure the shop hires experienced machinists who know CAD/CAM tools, and supported by engineers. Such collaboration on designs enhances manufacturability, reduces errors, and speeds project completion. Ask about their experience with intricate CNC machined parts and request references from comparable work.

Facility Scale, Machine Brands, And Capacity

Review the shop’s floor space, its lifting and heavy-load capacity, and the variety of machinery available. Spacious facilities equipped with advanced 5-axis machining centers, numerous CNC stations, and robust lifting mechanisms can handle big and sophisticated jobs. Opt for establishments signaling commitment to excellence through trusted brands including Hermle, DMG Mori, OKK, and Mitsubishi machines, helping ensure steady precision in CNC machining operations.

Customer Service, On-Time Delivery, And Industry-Specific Experience

Look for shops with ISO or AS9100 certification for work needing rigorous traceability. Shops that have demonstrated punctuality in delivery and that offer complete CNC machining solutions simplify operations, reducing handoffs and oversight needs. Select a collaborator providing thorough in-shop scrutiny, CMM assessments, and auxiliary processes to maximize quality control and efficiency.

Checklist:

  • Verified quality systems (ISO, AS9100)
  • Machine list showing 5-axis and horizontal capacity
  • Evidence of precision CNC machining and CNC machining services
  • References from your sector and on-time delivery performance
  • Internal inspection, assembly, and turnkey options

Final Thoughts

High-performing shops bring together broad capacity, capable teams, and modern equipment to keep CNC Precision Machining dependable across many sectors. From CAD/CAM-based prototyping through volume production, their precision machining minimizes errors and accelerates market readiness. An exemplary CNC machine shop combines milling, turning, and EDM. It undertakes stringent inspections to satisfy demanding standards across aerospace, medical, and energy industries.

ISO 9001 and AS9100 compliance, plus 5-axis machining and metrology expertise indicates a partner can handle strict tolerances and traceability demands. Custom CNC machining improves when engineers and machinists collaborate early to refine designs for manufacturability, supporting consistent quality. Turnkey integration services, paired with in-house CNC manufacturing reduce lead times and lower risk through centralized operations.

For U.S. businesses seeking dependable output, the selection of a partner should rest on tangible metrics of inspection systems, procedural documentation, and a proven track record in crafting complex components. An ideal CNC shop aligns technology, staff, and process excellence. This harmonization lays the groundwork for proficient CNC Precision Machining and sustained supply dependability.

Related: Why Quality Control Matters in a CNC Machine Shop in Houston

Read More About Injection Molds Houston For Accurate And Repeatable Production

Is it feasible for a single manufacturing process to offer complex shapes, high tolerances, and compounds that resist heat all at once? Welcome to a brief guide on a expandable production technology that renders complex, high-precision ceramic components possible. This technique blends fine powder with a binder to produce feedstock. That feedstock is then formed by injection, debound, and fired to near-theoretical density.

Learn more about bop inserts Houston

The key advantages comprise creative flexibility, consistency, close tolerances, and surface quality equivalent to metal working. The process excels specifically when tape casting or CNC have trouble with small, detailed parts.

Expect size variation from contraction during firing; early DFM thinking cuts redesign and expense.|Plan for dimensional shifts due to shrinkage during sintering; strategic design-for-process decisions cut cost and rework. The technology suits mid-to-high volume production where the investment in tooling and cycles makes financial sense.

Applications cover aerospace, automotive, healthcare equipment, electronics, and industrial components that demand abrasion, thermal, or corrosion resistance.|Sectors include automotive, aerospace, healthcare devices, tech, and industrial components requiring resilience to heat, wear, or rust. This guide guides the comprehensive process from materials selection through quality assurance and highlights modeling and measurement tools to secure reliable outcomes.

What Is Ceramic Injection Molding And Why It Matters Today

The injection molding process for micro-powder parts utilizes a plastic or wax binder mixed with powder to form a moldable feedstock.|Using a wax or thermoplastic binder mixed with powder, the injection molding method for fine parts creates a flowable feedstock. The mixture flows into complex cavities, yielding green parts with features difficult to create via dry pressing, slip casting, or isostatic pressing.

Comparison With Standard Methods

In contrast to slurry or pressing techniques, this route allows for inner passages, overhangs, and thin walls in small-to-mid-sized parts.|Contrary to powder compaction or slurry methods, this path enables thin walls, undercuts, and internal channels within small-to-medium components. Throughput is higher and variability is lower than manual processes.|Throughput is faster, and variance is lower compared to manual methods.

Its Place In Contemporary Workflows

Standard workflow: shrinkage design → mold making → injection → binder removal → firing → post-processing.|The usual sequence: design for shrinkage → tooling → molding → debinding → sintering → finishing. Production cycles frequently range from a few seconds to a several minutes per cycle.|Shot times typically run from seconds to minutes. The ideal volume is mid-to-high production where tooling investment pays off.

“Design validation through DOE trials and test batches reduces risk prior to mass manufacturing.”

Technique Geometry Speed Labor
CIM/MIM route High (overhangs, passages) High Minimal (automatable)
Slip casting Moderate Low Intensive
Isostatic/dry pressing Basic to medium Medium Moderate

Downstream, polishing or laser features can refine tolerances after sintering.|Downstream, laser features or lapping can tighten tolerances. This route meshes well with PPAP and SPC systems, boosting process control and traceability. The distinct advantages today include productivity, reduced scrap, and the capability to unlock designs that were otherwise too costly.

The Core Principles Of Ceramic Injection Molding

This section breaks down the step-by-step process that converts micro powder and binding agent into a dimensionally stable component prepared for sintering.|Here, we break down the step-by-step route converting fine powder and binder into a dimensionally stable part ready for sintering.

Converting Raw Materials To Components

Start by selecting powder with the right particle size distribution and surface characteristics.|Start with selecting powder having the right surface area and particle size distribution. These characteristics influence packing density, flow, and the final grain structure.

  • Blend the powder with a tailored binder system and process into feedstock with desired solids loading (usually 55–65 volume percent).
  • Use molding to create a green body; focus on gate placement to prevent weld lines and inconsistent packing.
  • Debind to yield a delicate brown body, then fire to near-theoretical density.

Binding agents must move for good mold filling, hold shape during processing, and leave cleanly during binder removal to avoid blisters or fractures.|Binders must flow to fill well, hold shape during handling, and exit cleanly during debinding to prevent cracks or blisters.

Material rheology — thickness vs. heat and stress — dictates fill behavior, weld lines, and surface quality.|Feedstock rheology — viscosity against shear and temperature — governs fill behavior, surface finish, and knit lines. CIM machine geometry and screw configuration ensure feedstock homogeneity and stop breakdown.|Machine geometry and screw/barrel design in CIM protect feedstock homogeneity and prevent degradation.
cast inserts Houston

“Control the process parameters: small variations in temperature or force frequently lead to incomplete fills, air pockets, or bad surface quality.”

Compared with MIM, this route uses higher firing temps and distinct gas environments to suit material chemistry and densification requirements.|Compared to MIM, this route uses different atmospheres and higher sintering temperatures to match densification needs and ceramic chemistry.

Preparing Materials And Feedstock For Precise Ceramics

Selecting the correct powders and binders lays the groundwork for predictable, high-precision parts.|The foundation for predictable, high-precision parts is set by selecting the right binders and powders.

Selecting Powders And Critical Specifications

Alumina is ideal when wear resistance and dielectric strength are required.|Alumina excels where electrical insulation and wear resistance matter. Zirconia provides toughness for impact-prone parts.|Zirconia adds fracture toughness for parts prone to shock. SiC suits high-temperature and harsh conditions.|Silicon carbide suits abrasive and high-temperature environments.

Manage grain size, shape, and purity.|Control purity, shape, and particle size. Fine, spherical powder enhances packing and surface finish.|Spherical, fine powder improves surface finish and packing. Non-spherical shapes can increase green strength but may roughen the finished surface.|Irregular particles can boost green strength but may roughen the final surface.

Binder Types And Proportions

Typical binder families encompass waxes and polyolefins like PE and polypropylene, plus additives for complex shapes.|Common binder families include polyolefins such as polypropylene and polyethylene, waxes, plus specialty polymers for difficult shapes. Binder percent affects melt flow and removal speed.|Debinding time and melt flow are affected by binder percent.

Rheology And Compounding

Mix with a consistent order: dry mixing, slow polymer addition, followed by regulated temperature and shear.|Compound using a steady sequence: dry powder blending, gradual polymer addition, then controlled shear and temperature. Avoid binder degradation by controlling peak temperatures.|Limit peak temperatures to prevent binder degradation.

Analyze material with rheometers or torque rheometers to verify flow ranges for reliable filling and compaction.|Test feedstock using torque rheometers or capillary rheometry to confirm viscosity windows for reliable packing and fill. Target powder loading that optimizes solidness and shrinkage — usually about 55–65 vol% for dense components.|Aim for solids loading balancing shrinkage and density — typically around 55–65 vol% for high-density parts.

Procedures For Storage, Handling, And Drying

Store materials in sealed containers and follow FIFO.|Store powders in sealed containers and use FIFO. Control humidity for moisture-sensitive additives and dehumidify feedstock prior to injection to reduce voids and defects.|Dry pellets before molding and control humidity for hygroscopic additives to reduce blemishes and voids.

Follow PPE and dust management when working with fine powder and hot polymers.|When handling hot polymers and fine powder, follow dust controls and PPE. Upfront supplier collaboration on powder and binder choices speeds approval and lowers iteration risk.|Early supplier collaboration on binder and powder choices lowers iteration risk and speeds validation.

Designing Parts For Injection Molding

Engineering for this route starts with defined objectives: meet specs and reduce finishing.|Designing for this route starts with clear goals: meet tolerances and limit post-sinter work. Early CAD decisions influence contraction, strength, and manipulation of fragile green components.|Early CAD decisions control shrinkage, strength, and handling of fragile green components.

Thickness, Gating, And Knit Line Control

Keep wall thickness consistent and use smooth tapers to minimize dimples and distortion.|Keep wall thickness uniform and use gradual transitions to reduce sink and warpage. Position gates so material flows from cosmetic or high-stress areas to avoid weld lines in key areas.|Place gates so flow moves away from high-stress or cosmetic areas to avoid knit lines in critical zones.

Add a shrinkage factor and resize key features in the mold to hit final dimensions.|Add a shrink map and scale key features in the mold to hit final dimensions. Validate with flow simulation and a DFM review before tooling.|Validate with flow simulation and a DFM review before tooling.

Features For Debinding/Sintering, Draft, And Radii

Include modest tapers and ample curves to facilitate demold and reduce stress points.|Provide modest draft angles and generous radii to ease demold and lower stress concentrations. Integrate vents, sacrificial channels, or setters to speed debinding and support fragile shapes.|Integrate vents, sacrificial channels, or setters to speed debinding and support fragile shapes.

Specify reference planes and measurement spots that align with the way components are held during firing and QC.|Define datums and inspection points that match how components are fixtured during sintering and QC. Leave minimal finishing stock for critical fits but preventing excess that raises cost.|Allow minimal finishing stock for critical fits while avoiding excess that raises cost.

Focus Area Suggestion Advantage Check
Wall thickness Uniform, gradual transitions Less warp; predictable shrinkage Modeling / Sample
Gating location Out of cosmetic/stress zones Reduced knit lines Flow sim
Removal aids Passages, supports Safer brown parts; fewer cracks Design check

Tooling And Mold Considerations For Ceramic Injection

An engineered mold set reduces scrap and enhances dimensional control across high volume runs.|A well-designed toolset reduces scrap and improves dimensional control across long production runs. Begin by material choices and coatings to handle gritty material and close specs.|Start with material choices and surface engineering to handle abrasive feedstock and tight tolerances.

Mold materials must resist wear and thermal cycling.|Mold materials should resist abrasion and thermal cycling. Choose high-performance steels or superalloys and apply wear-resistant coatings for extended tool life.|Select high-performance steels or nickel-based alloys and add wear-resistant coatings for extended tool life.

Optimize surface finish to assist ejection whilst preserving detail.|Balance surface finish to aid release while preserving detail. Avoid textures that trap binder or lead to adhesion.|Avoid textures that trap binder or cause sticking. Engineer air vents to clear gas and fumes and prevent burn marks or short shots.|Engineer venting to clear air and volatiles and prevent burn marks or short shots.

  • Select gating styles (side, submarine, hot tip) and channels to promote balanced filling and minimize weld lines.
  • Refine water lines to maintain cavity temperature and reduce process drift.
  • Use robust ejection—plates or air blast—to protect fragile green parts upon ejection.
  • Fit swappable components for quick iteration on inlets, vents, and key tolerances.
  • Account for tolerance stack-ups by adjusting molds for expected shrinkage.
  • Install internal pressure and thermocouples to monitor the process and allow closed-loop control.
  • Plan maintenance intervals and wear checks to keep quality consistent over long runs.

These measures tighten dimensional control and lower downstream rework.|These measures tighten dimensional control and reduce downstream rework. Furthermore, they enable volume manufacturing using modern molding technology whilst safeguarding tool investment.|They also support scalable production using modern molding technology while protecting tool investment.

Running The Injection Molding Phase Step-By-Step

A repeatable molding cycle relies on thermal profiles, pressure ramps, and operator discipline.|A repeatable press cycle depends on temperature maps, pressure ramps, and operator discipline. Begin with a clear setup list that safeguards feedstock and equipment from thermal shock.|Start with a clear start-up checklist that protects feedstock and machine from thermal shock.

Machine Setup: Temperature, Pressure, And Injection Speed

Set cylinder and thermal settings to keep flow constant without burning the polymer.|Set barrel and mold temperature profiles to keep viscosity stable without degrading the binder. Dial in injection speed and pressure ramps to fill complex features whilst avoiding splaying and flow lines.|Dial in injection speed and pressure ramps to fill complex features while avoiding jetting and flow lines.

Filling, Packing, And Cooling For Tight Tolerances

Employ multi-stage packing to densify green parts and eliminate internal voids.|Use multi-stage packing to densify green parts and reduce internal voids. Balance chill time for handling strength and speed.|Balance cooling time for handling strength and cycle efficiency. Use cleaning and material changeover steps to prevent cross-contamination.|Implement purging and material changeover steps to avoid cross-contamination.

Ejecting Green Parts Without Damage

Use low-friction coatings and controlled release agents where needed.|Apply low-friction coatings and measured mold release where needed. Use controlled ejection and soft handling for delicate features.|Use controlled ejection and guarded fixtures for delicate features. Train operators to identify defects quickly and halt the production if required.|Train operators to spot defects early and stop the run if needed.

Parameter Target Outcome
Temperature settings Consistent flow range Less short shots; good finish
Pressure & speed ramps Programmed multi-stage Complete fill; reduced weld lines
Packing & cooling Staged; optimized duration Even density; stable dimensions

Best Practices And Methods For Debinding

Successful debinding is a critical step that converts a fragile molded part into a furnace-ready item.|Effective binder removal is a critical step that turns a fragile green part into a sinter-ready component.

Two main debinding methods are standard: chemical debinding and thermal debinding.|Two main debinding methods are common: solvent debinding and thermal debinding. Solvent debinding extracts the soluble components initially.|Solvent debinding extracts the soluble binder fraction first. Heat removal then burns off the residual binder by controlled pyrolysis.|Thermal debinding then removes the remaining polymer by controlled pyrolysis.

Thermal Vs. Solvent Methods

Solvent processing is fast for soluble phases and lowers gas pressure during the next stage.|Solvent debinding is fast for soluble phases and reduces internal pressure during the next stage. Thermal processing is more time-consuming but necessary to eliminate hard-to-dissolve polymer.|Thermal debinding is slower but needed to remove hard-to-dissolve polymer. Selecting the correct approach relies on binder chemistry and part geometry.|Choosing the right method depends on binder chemistry and part geometry.

Preventing Defects In Debinding

Support selection and positioning are crucial.|Fixture choice and part orientation matter. Support weak spots and allow free escape paths for gases to prevent fractures and warping.|Support fragile areas and allow free escape paths for volatiles to prevent cracking and distortion.

Use slow heat-up rates, staged hold times, and air circulation to avoid pressure spikes that cause blistering.|Use gentle heating ramps, staged hold times, and controlled airflow to avoid pressure spikes that cause blistering. Heavy walls and deep pockets need longer cycles or venting.|Thick sections and blind holes need longer cycles or local vents.

Select solvents with recycling units and proper ventilation.|Pick solvents with recovery systems and proper ventilation. Follow safety sheets and regulations to safeguard staff and meet laws.|Follow MSDS guidance and local environmental rules to protect workers and comply with regulations.

  • Run test coupons and test pieces to verify complete debinding before sintering.
  • Look for odor, discoloration, or unexpected mass loss profiles—these indicate leftover binder.
  • Troubleshoot skin formation, layer separation, or slump by slowing ramps, venting better, or changing fixture layout.

Debinding success ties back to molding and injection quality; bubbles or knit lines frequently turn into cracks in removal.|Debinding success ties back to molding and injection quality; voids or knit lines often become failure points during removal. Record profiles and weight data to standardize production and ensure final part quality.|Record debinding curves and mass loss data to standardize processing and protect final part quality.

Sintering To Final Density And Performance

Precision sintering is the process that converts a fragile brown shape into a dense, service-ready part.|Controlled sintering is the step that converts a fragile brown shape into a dense, service-ready part. The furnace cycle sets microstructure, porosity, and mechanical properties that determine long-term performance.

Controlling Shrinkage, Atmospheres, And Temperature

Use a three-step cycle: gentle heating to burn off leftover binder, a controlled ramp into the sintering zone, and a controlled cooling to prevent cracking.|Use a three-stage profile: slow heat-up to remove residual binder, a controlled ramp into the densification range, and a measured cool-down to avoid thermal shock.

Align atmosphere to material: oxygen for oxides, inert or hydrogen for non-oxides and some engineered mixes.|Match atmosphere to material: air for alumina-type oxides, inert or reducing for carbides and some engineered mixes. The right gas preserves chemistry and color while limiting grain boundary reactions.

Measure shrinkage with sacrificial coupons and feed data back to cavity compensation.|Measure shrinkage with sacrificial coupons and incorporate those values into cavity compensation. Design setters and supports to restrain distortion and permit uniform gas flow.|Design setters and supports to restrain warpage and allow uniform gas flow.

Achieving Strength, Corrosion Resistance, And Wear Resistance

Sintering changes crystal size and voids, which drive bending strength and toughness.|Sintering alters grain size and porosity, which drive flexural strength and fracture toughness. Target full density with low grain coarsening to meet mechanical targets.|Aim for high density with minimal grain coarsening to meet mechanical targets.

Choose material chemistry and dwell times to maximize chemical resistance and surface hardness for wear resistance.|Select material chemistry and sinter soak times to optimize corrosion resistance and surface hardness for wear resistance. Evaluate post-sinter HIP if micro-pores impacts fatigue or hermeticity.|Consider post-sinter HIP where residual porosity affects fatigue or sealing.

  • Document profiles and utilize thermocouples or pyrometry to validate heat accuracy.
  • Control loading and gaps to ensure even temperature and atmosphere exposure.
  • Watch for defects: sagging, large grains, and voids—slower heating and fixtures frequently fix these.
Parameter Target Impact on Properties Production Tip
Heating rate 1–5 °C/min (debind) / 5–20 °C/min (fire) Reduces cracking; controls grain growth Align with mass/binder
Dwell settings Material dependent; varied time Densification; pore removal Use samples to verify
Atmosphere Air / inert / reducing Preserves chemistry; prevents oxidation Check flow and purity
Post-sinter options HIP/Annealing Remove pores; increase strength Apply when parts need max performance

“Consistent firing cycles and calibrated ovens directly raise output and cut secondary work.”

QC, Measurements, And Tolerances

A robust QC plan converts variability in shrinkage into predictable tolerances.|A robust metrology plan turns uncertainty in shrinkage into predictable tolerances. Begin with defined checkpoints at green, brown, and sintered states to catch errors sooner.|Start with clear inspection gates at green, brown, and sintered states to catch deviations early.

Measuring Shrinkage And Compensating In The Mold

Use shrinkage correlation charts from trials to scale cavity dimensions.|Use shrinkage correlation charts from pilot runs to scale cavity dimensions. Validate with sacrificial coupons and refine the tooling offsets before full tooling runs.|Validate with sacrificial coupons and update the mold compensation map before full tooling runs.

Surface Quality, Microstructure, And Porosity Checks

Check roughness and specific gravity using profilometers and Archimedes testing.|Inspect surface finish and density using profilometers and Archimedes testing. CT scans and optical scans show voids that impact mechanical properties.|Micro-CT and optical scans reveal internal pores that affect mechanical properties.

  • Establish inspection plans covering green, brown, and sintered states with criteria.
  • Apply metrology: CMM, optical scanners, surface profilometers, micro-CT for internal verification.
  • Link microstructure and porosity with strength and wear performance.
Stage Instrument Measurement Action
Molded parts Vision system Dimensions Adjust mold compensation
Debound parts X-ray Void distribution Modify debind cycle
Sintered parts CMM / Surface check Specs / Roughness Approve lot
Batch control SPC software Capability / Density Hold or release lots

Deploy SPC and process studies prior to PPAP.|Implement SPC and capability studies before PPAP. Keep records from lot-level raw materials through batches.|Maintain traceability from lot-level powders and binders through batches. Check tools, perform measurement analysis, and define reject procedures with root-cause action plans.|Calibrate gauges, run MSA, and define nonconformance flows with root-cause action plans.

“Reliable measurement and records close the loop on manufacturing quality.”

Applications In The US Market

US manufacturers prefer CIM when components need to merge low mass and durability.|Domestic producers favor feedstock-based production when parts must combine low mass and high wear resistance. Across aviation, automotive, healthcare, and tech, vendors use this route to hit tight specs and harsh environments.|Across aerospace, automotive, medical, and electronics, suppliers use this route to meet tight specs and harsh environments.

Aerospace Applications: Lightweight Strength

In aerospace, manufacturers specify lightweight bearings, jets, and thermal barrier parts that demand efficiency.|In aerospace, manufacturers specify lightweight wear components, nozzle inserts, and thermal barrier parts that demand high strength-to-weight performance.

These parts improve MPG and withstand temperature cycling and vibration in turbines and actuation systems.|These components improve fuel efficiency and survive temperature cycling and vibration in engines and actuation systems.

Automotive Uses: Durability And Heat Resistance

Car applications include pump components, casings, and exhaust parts that require thermal stability and longevity.|Automotive use cases include pump components, sensor housings, and exhaust-related insulators that need thermal stability and long-term durability.

Swapping steel parts for ceramic parts reduces corrosion and extends service life in tough engine bays.|Swapping metal parts for engineered powdered parts reduces corrosion and extends service life in harsh under-hood environments.

Medical/Electronics: Small, Precise Parts

Medical and electronics markets benefit from tiny insulators, ferrules, implantable device components, and biocompatible wear parts.|Medical and electronics markets benefit from micro-scale insulators, ferrules, implantable device components, and biocompatible wear parts.

These components need precision, insulation, and validated biocompatibility or dielectric testing prior to launch.|These components require tight tolerances, dielectric performance, and validated biocompatibility or dielectric testing prior to production release.

  • Performance advantage: excellent wear resistance and chemical resistance make these components perfect for harsh service.
  • Certified manufacturing often adheres to AS9100, auto standards, or ISO 13485 with records and tracking.
  • Design-for-assembly is key for assemblies that join these parts to metals or plastics.
Stage Lead Time Comment
Mold to Sample 6–12 weeks Depends on insert complexity
Pilot to SOP 1 – 2 months Validation and qual testing
Overall 2.5 – 5 months Local supply helps speed

Qual steps include biocompatibility studies for medical parts and electrical tests for devices.|Validation steps include biocompatibility studies for implants and dielectric testing for electronics. Numerous cases show this method substituting metal parts to cut weight and remove corrosion failure modes in service.|Many success stories show this approach replacing metal designs to cut weight and remove corrosion failure modes in service.

Cycle Times, Costs, And CIM Vs. Machining

Knowing costs helps decide whether CIM or CNC is the smarter path.|Understanding economics helps decide whether formed-powder production or machining is the smarter path. Start by mapping the main cost drivers and how speed impacts cash flow.|Start by mapping the main cost drivers and how cycle time affects cash flow.

Major Expense Drivers

Molds and mold depreciation frequently dominate initial spend.|Tooling and mold amortization often dominate initial spend. High-performance steels or interchangeable inserts increase up-front cost but reduce unit cost over volume.|High-performance steels or interchangeable inserts raise up-front cost but lower per-piece cost over volume.

Raw material, press time, sintering time, labor, and yield losses contribute to final cost.|Material/feedstock, press time, furnace soak, labor, and yield losses all add to true landed cost. Post-processing, inspection, and packaging also matter.|Secondary finishing, inspection, and packaging also matter.

Factor Impact How to reduce
Tooling / mold High CapEx; low OpEx Modular inserts; amortize over volume
Materials Variable cost; impact on yield Bulk buy; optimize mix
Machine & furnace time Sets throughput and cash flow Balance press cycle with sinter batch size
Scrap rate Profit killer Good design habits

CIM Advantages Over Machining

For complex geometry and volume production, unit costs fall below CNC.|For complex geometry and mid-to-high volumes, per-part costs fall below machining. Cutting hard ceramics generates waste and long cycle times for internal channels.|Machining brittle blanks creates much scrap and long cycle times for internal channels.

Machining still wins for very low volumes, oversized pieces, or if tolerances require tight post-sinter finishing.|Machining still wins for very low volumes, oversized pieces, or when tolerances need tight post-sinter finishing.

“Smart design and scheduling convert fixed costs to competitive per-part pricing.”

Heuristics For Quoting

  • Calculate tooling payback: tooling cost ÷ expected units = tooling per-part.
  • Add feedstock, machine time, furnace pro rata, work, QA, and pack to get piece price.
  • Include a scrap buffer (5–15%) and a finishing cost.

These steps outlines TCO and reveal where design, process choices, and smarter tooling deliver the greatest advantages.|These steps frame total cost of ownership and show where design, process choices, and smarter tooling deliver the biggest advantages.

Solving Common CIM Defects

Finding the root cause of short shots or warpage needs a mix of metrics and logic.|Finding the real cause of short shots or warpage needs both data and structured problem-solving. Follow a basic checklist to separate problems that originate in injection, binder removal, or sintering.|Use a simple checklist to separate problems that start in molding, debinding, or sintering.

Diagnosing Typical Defects

Incomplete fills occur if fill speed or pressure is insufficient, air vents are blocked, or material contains water.|Short shots and voids happen when injection speed or pressure is too low, vents are blocked, or feedstock carries moisture.

Distortion frequently comes from bad packing, uneven cooling, or poor support in the furnace.|Warpage often traces to unequal packing, nonuniform cooling, or poor support during sintering.

Delamination and bad welds respond to new gates, hotter material, or flow balancing across cavities.|Delamination and weak knit lines respond to gate redesign, higher melt temps, or flow balancing across cavities.

  • Blisters or cracks: slow ramp rates, uneven part mass, or poor solvent penetration.
  • Inspect mold wear and surface damage if defects start after high volume.
  • Use incoming inspection to control feedstock variability and humidity.

“Apply structured root-cause tools such as Ishikawa and the 5-Whys to find stage-specific failures.”

Defect Likely Cause Fast Action
Short shot/void Low pressure/speed, poor venting Increase injection pressure; clear vents
Distortion Uneven packing/cooling Balance fill; adjust cooling
Cracking Debind profile issues Slower heat; check solvent

Perform experiments to optimize settings and confirm solutions.|Run DOE to tune parameters and verify fixes. Monitor failure codes and Pareto charts to target actions.|Track defect codes and Pareto charts to focus improvements. Close the loop among press operators, furnace techs, and QA to shorten fix time and raise yield in the plant.|Close the loop between press operators, furnace techs, and QA to shorten time-to-correct and raise overall quality in the process.

Safety, Compliance, And Sustainable Processing

Safeguarding workers and the environment is as important as meeting specs in modern manufacturing.|Protecting workers and the environment is as important as hitting tolerances in modern powder-based production.

Safety With Powders And Binders

Wear PPE: N95 or P100 respirators, gloves, glasses, and protective clothing for dry powder and binder handling.|Use PPE: N95 or P100 respirators, chemical-resistant gloves, eye protection, and protective clothing for dry powder and hot binder work.

Use local exhaust ventilation and filters to control airborne powder.|Install local exhaust ventilation and HEPA filtration to control fugitive dust. Enclose hoppers and use grounded transfer lines to reduce sparks.|Enclose transfer points and use grounded transfer lines to reduce static risks.

“Train staff on spill response, chemical safety, and safe storage—regular drills ease inspections.”

Energy, Recycling, And Waste Management

Segregate waste streams: powder waste, used binder, chemicals, and garbage.|Segregate waste streams: loose powder, used binder, solvent residues, and general refuse. Label bins and keep solvent and powder streams separate for recycling.|Label containers and keep solvent and powder streams separate for recovery.

Implement closed-loop solvent recovery and controlled feedstock regrind if allowed.|Adopt closed-loop solvent recovery and controlled feedstock regrind where quality permits. Doing so lowers disposal costs and saves feedstock.|This reduces disposal costs and preserves raw materials.

Schedule furnace loads to fill the kiln and minimize peak demand.|Schedule furnace loads to maximize fill and minimize peak demand. Improve lining, use high-efficiency motors and VFDs, and log energy data for ISO 14001-style efficiency.|Improve insulation, use high-efficiency motors and variable-speed drives, and log energy data for ISO 14001-style continuous improvement.

Comply with OSHA and environmental rules for hazardous air pollutants, solvent emissions, and recordkeeping.|Follow OSHA and EPA rules for hazardous air pollutants, solvent emissions, and recordkeeping. Keep SOPs, logs, and MSDS ready for inspectors.|Keep documented procedures, training records, and material safety data sheets ready for audits.

Engineer parts to reduce weight and processing time—these actions lower power and offer clear environmental advantages while keeping manufacturing steady.|Design parts to cut mass and cycle time—these simple choices lower energy use and offer clear environmental advantages while keeping production reliable.

Taking Your Ceramic Injection Molding Project To Production

Convert concepts into reliable production by sequencing material trials, tool proofs, and pre-production.|Turn design intent into reliable production by sequencing material trials, tool proofs, and pilot runs.

Practical checklist: select material, run a DFM review, run simulation, make prototype tool, validate, and execute approval or equivalent.|Practical checklist: pick feedstock, run a DFM review, simulate flow, build a prototype mold, complete validation runs, then execute PPAP or equivalent.

Establish milestones from Quote → proto mold → studies → FAI → Start of Production.|Set milestones from RFQ → prototype tool → capability studies → first article inspection → SOP. Agree requirements and timelines with suppliers to de-risk decisions.|Agree deliverables and timelines with suppliers to de-risk early choices.

Record quality plans, SOPs, and quality metrics before launch.|Document control plans, work instructions, and quality metrics before pilot production. Plan capacity for press tonnage, furnace volume, debind throughput, and staffing.|Plan capacity for press tonnage, furnace volume, debind throughput, and staffing.

Aim for early wins in which accuracy and complex geometry create value.|Target early wins where precision and complex geometry add value. Sustain consistency with PM, gauge R&R, and audits.|Maintain quality with preventive maintenance, gauge R&R, and periodic requalification.

Ready to proceed? Ask for a feasibility review and a quote using your parts, quantities, and performance needs.|Ready to proceed? Request a feasibility review and a cost model based on your parts, volumes, and performance needs.

Common Questions

itemprop=”name”>What is the process behind making precision ceramic parts with injection techniques?

The method starts by mixing ceramic or carbide powder with a binder to create a homogenous feedstock.|The process starts by mixing fine oxide or carbide powder with a polymer-based binder to form a homogenous feedstock. The mixture is shot into a mold under pressure to create a green part.|That feedstock is shot into a mold under pressure to create a green part. After molding, the polymer is removed via solvent or thermal debinding, and the part is sintered to achieve full density and mechanical properties.|After molding, the binder is removed through solvent or thermal debinding, and the part is sintered to reach final density and mechanical properties. Every step — mixing, molding, debinding, and firing — must be controlled to hit tight tolerances and quality goals.|Each stage — compounding, molding, debinding, and sintering — must be controlled to meet tight tolerances and material performance targets.

itemprop=”name”>CIM vs. traditional forming: What’s the difference?

In contrast to dry pressing or casting, which shape items one at a time or need finishing, CIM enables mass production of complex shapes with details and consistent repeatability.|Unlike pressing or slip casting, which shape parts one at a time or require significant machining, injection enables high-volume production of complex geometries with fine features and consistent repeatability. It also reduces grinding for most parts, improving yield and reducing unit cost in volume.|It also reduces post-sintering machining for many components, improving material yield and lowering per-part cost at scale.

itemprop=”name”>Common materials for CIM parts?

Typical materials are aluminum oxide, zirconia, and SiC.|Common powders include alumina, zirconia, and silicon carbide. Carbides are used when hardness matters.|Tungsten carbide blends appear where extreme wear resistance matters. Powder selection depends on strength needs, thermal stability, corrosion resistance, and electrical properties.|Powder selection depends on required strength, thermal stability, corrosion resistance, and electrical properties. Proper chemistry and particle size distribution also affect feedstock flow and final density.|Proper powder surface chemistry and particle size distribution also affect feedstock flow and final density.

itemprop=”name”>What role do binders play and how are they chosen?

Binding agents provide strength and flow during molding, then must be removable avoiding damaging the part.|Binders provide cohesion and flow during molding, then must be removable without harming the part. Typical systems employ wax and plastics in controlled ratios to balance viscosity, handling strength, and debinding behavior.|Typical systems use waxes and polymers in controlled ratios to balance viscosity, green strength, and debinding behavior. Selection relies on shape, debinding method, and environmental or safety requirements.|Selection depends on part geometry, debinding method, and environmental or safety requirements.

itemprop=”name”>Design strategies for shrinkage and tolerances?

Engineers compensate by sizing mold cavities to counteract expected shrink during sintering.|Designers compensate by scaling mold cavities to offset predictable linear shrinkage during sintering. Also, they manage walls, fillets, and locate gates to minimize knit lines and deformation.|They also control wall thicknesses, add radii, and locate gates to minimize knit lines and deformation. Working closely with the molder helps set achievable tolerances based on material and process capability.|Close collaboration with the manufacturer helps set achievable tolerances based on material and process capability.

itemprop=”name”>How does the mold affect CIM part quality?

Tool steel, polish, venting, and gating all influence fill, packing, and demolding.|Mold material, surface finish, venting, and gate and runner design all influence filling, packing, and demolding. Tough steels with polished cavities reduce surface defects.|Hardened steels with polished cavities reduce surface defects. Good venting stops air pockets and mis-runs, whereas good gates produce consistent feedstock flow and limit knit lines.|Proper venting prevents trapped gas and short shots, while optimized gates yield consistent feedstock flow and reduce weld lines.

itemprop=”name”>Optimizing molding for precision dimensions?

Settings — barrel and mold temperature, injection speed, and holding pressure — are tuned to ensure complete cavity fill and consistent packing.|Machine parameters — barrel and mold temperature, injection speed, and holding pressure — are tuned to ensure complete cavity fill and consistent packing. Cooling and demolding timing are set to avoid distortion of parts whilst maintaining speed.|Cooling and demolding timing are set to avoid distortion of green parts while maintaining cycle efficiency. Monitoring metrics helps reduce variance.|Monitoring process data helps keep variation low.

itemprop=”name”>When to use solvent vs thermal debinding?

Chemical debinding extracts soluble binder fractions and is gentle for complex features.|Solvent debinding extracts soluble binder fractions and is gentle for complex features. Heat debinding ramps temperature to burn off or pyrolyze the rest and is often applied after solvent wash.|Thermal debinding ramps temperature to evaporate or pyrolyze the remainder and is often used after solvent steps. The choice depends on binder chemistry, wall size, and risk of defects.|The choice depends on binder chemistry, part thickness, and risk of cracking or blistering.

itemprop=”name”>How do manufacturers avoid defects like cracking or blistering during debinding?

Manufacturers control ramps, ensure venting paths, and use staged solvent/thermal sequences matched to feedstock.|They control heating rates, ensure venting paths, and use staged solvent/thermal sequences tailored to feedstock. Uniform binder removal and reducing internal pressure during decomposition lower stresses that create failures.|Uniform binder removal and minimizing internal pressure during decomposition reduce stresses that cause cracks or blisters.

itemprop=”name”>Best sintering practices for material properties?

Furnace cycles — temperature, soak, ramp rates, and atmosphere — are tuned for shrinkage whilst limiting coarsening.|Sintering profiles — temperature, hold time, ramp rates, and atmosphere — are optimized for densification while limiting grain growth. Specific gases or isostatic post-sinter densification are used to reach full density, strength, and finishes such as durability.|Controlled atmospheres or isostatic post-sinter densification may be used to achieve target density, strength, and surface properties like wear and corrosion resistance.

itemprop=”name”>Measuring and guaranteeing quality in CIM?

QC employs dimensional inspection adjusted for shrinkage, microstructure analysis, density checks, and strength testing.|Quality control uses dimensional inspection adjusted for shrinkage, microstructure analysis, porosity checks, and mechanical testing. Statistical process control tracks variables to maintain consistency, and FAI confirms tooling compensation and results.|Statistical process control monitors key parameters to maintain repeatability, and first-article inspection validates tooling compensation and sintering outcomes.

itemprop=”name”>Top sectors for ceramic injection molding?

Aerospace, automotive, medical devices, and tech are key users.|Aerospace, automotive, medical devices, and electronics benefit most. Common applications are wear parts, strong parts needing precision, and miniature parts when machining would be impractical or costly.|Typical uses include thermal or wear-resistant components, high-strength parts requiring tight geometries, and miniature parts where machining would be impractical or costly.

itemprop=”name”>CIM vs Machining: When is CIM cheaper?

It pays off as volumes rise, shapes are complex, or part consolidation reduces assembly.|It becomes economical when volumes rise, geometries are complex, or part consolidation reduces assembly steps. Mold cost is spread over many parts, and the reduced need for machining lowers scrap and unit cost.|High tooling cost is amortized over many parts, and the reduced need for machining lowers material waste and cycle cost per component.

itemprop=”name”>What common molding defects should teams watch for and how are they diagnosed?

Short shots, holes, bending, and peeling are caused by material issues, bad venting, incorrect process settings, or bad processing.|Short shots, voids, warpage, and delamination can stem from feedstock problems, poor mold venting, incorrect process settings, or improper debinding/sintering. Troubleshooting links flaws to stage, then isolates variables like force, heat, or flow for fixing.|Root-cause analysis maps defect location to process step, then isolates variables like pressure, temperature, or feedstock rheology for correction.

itemprop=”name”>Handling powders/binders: Safety rules?

Employ ventilation, dust controls, and gear when using particulates.|Use local exhaust ventilation, dust controls, and appropriate PPE when handling fine powders. Dispose of chemicals according to OSHA and EPA guidelines.|Manage solvent and binder waste per OSHA and EPA guidelines. Recycling of scrap feedstock and energy-efficient sintering lower impact.|Recycling of scrap feedstock and energy-efficient sintering reduce environmental footprint.

itemprop=”name”>How should a company begin if they want to move a prototype to production?

Begin with choosing materials and a DFM review.|Start with material selection and a design review for manufacturability. Run pilot parts to test material, mold compensation, and sintering.|Produce pilot parts to validate feedstock, mold compensation, and thermal profiles. Refine tooling and process parameters, and scale with qualified suppliers who can show measurements and control.|Iterate tooling and process parameters, then scale with qualified suppliers who can demonstrate consistent metrology and process control.

Related: Solutions for High-Volume Production in Industrial Molds Houston

Resilient Seated Gate Valve Bonnet Designs

Cast-Iron Gate Valves: Key Features, Advantages, and Applications

Could a single, well-made valve cut maintenance time and keep water systems running longer?

I manufacture and supply Cast Iron Gate Valve Manufacturer at Yaxing Valve, and I back their build quality and support for U.S. customers. This line is engineered for longevity in waterworks and light-industrial systems.

Each gate valve has a robust iron body, a machined wedge path, and straightforward handwheel operation. The result is dependable shutoff, simple maintenance, and consistent performance in buildings, fire mains, and utility distribution lines.

I work with specifiers to speed submittals and deliver clear details: sizes, connection types, pressure classes, and optional accessories. We retain cart and preference data (cookies) to make reorders simple.

If you need a practical replacement or a cost-effective option for new projects, compare these cast-iron gate valve advantages against your current hardware to see lifecycle value and real-world fit.

Why Yaxing Valve Cast Iron Gate Valves Deliver Reliable Flow Control

I verify each Yaxing Valve product myself to confidently recommend it for demanding U.S. applications.

Rugged cast-iron body engineered for industrial performance

Every valve features a strong cast-iron body that resists load-induced deformation. Metal-to-metal seating and precise machining ensure tight shutoff when customers need it most.

Cast Iron Gate Valve Manufacturer

Shaped for maximum flow and low pressure drop

The internal path is optimized to lower turbulence and pressure loss. That helps pumps run more efficiently and lowers energy use across systems.

  • I validate product dimensions and testing to align with common ANSI standards and internal checks.
  • I refine stem/wedge/bonnet interfaces to reduce friction and maintain consistent torque over time.
  • I set body thickness targets for durability while keeping weight manageable for installers.
  • Documentation lists tests/standards so purchasing can wrap orders quickly.
Key Feature Primary Benefit Tech Note
Cast-iron body Strong structural integrity Meets dimensional stability targets
Optimized gate geometry Reduced pressure drop Boosts pump operating efficiency
Finished stem/handwheel interfaces Smoother operation Steady torque over service life
Test documentation Speedier submittal clearance ANSI-referenced reports

Cast Iron Gate Valves: Materials, Design, and Performance Essentials

I outline the body, sealing, and stem choices to make selection and ordering straightforward.

Body, bonnet, and wedge materials

Material stack-up: cast-iron body and bonnet, precision-machined wedge, metal-to-metal seat interface for dependable isolation across water service and general industry.

Stem and Handwheel Options

I offer non-rising stem and inside screw stems for compact installations. Screw thread forms and packing arrangements are fully documented.

Performance limits and standards

I provide qualified pressure/temperature ranges and ANSI-aligned end connections so engineers can confirm fit without extra drawings.

  • Interface between stem and handwheel tuned for consistent torque.
  • Smooth internal geometry reduces headloss.
  • Series identifiers and submittal-ready specs speed ordering and approvals.
Item Material/Type Rating Notes
Valve body/bonnet cast iron 150 psi ANSI flange dimensions, welded/bolted options
Gate wedge Machined metal −20°–180°F range Metal-to-metal seating, low headloss finish
Operating stem Non-rising / inside screw N/A Documented thread and packing in datasheet
Model series YX-100 and YX-200 2″ to 12″ sizes Simple part numbering

Modern Applications, Install, and Operation

I help contractors and owners place these valves where they perform best in modern loops. The goal is straightforward selection, installation, and checks so crews complete commissioning without callbacks.

Use cases: waterworks, building systems, general industry

Select full-port units for low restriction across long mains, service feeds, and bypass lines.

For mechanical rooms and industrial loops with limited headroom, I favor non-rising stem or inside-screw designs.

Installation guidelines

Protect the body during handling by lifting at rated points and avoiding flange stress. Confirm alignment prior to final torque to prevent distortion/leaks.

Choose media-compatible gaskets, use a cross-torque sequence, and provide supports to prevent sag.

Operation & maintenance notes

Position the handwheel for easy access and verify free movement after packing tweaks.

Perform periodic torque checks under pressure, inspect the wedge and packing, and confirm the pressure/temperature range against your media. Capture tag IDs in your account and link CMMS work orders.

Topic Action When Result
Use-case mapping Select full-bore for mains; non-rising for tight spaces Design stage Reduced headloss and saved space
Handling/installation Lift properly, align, then cross-torque bolts Field install Prevents leaks and flange distortion
Commissioning checks Confirm handwheel feel; perform pressure tests Startup and routine Stable operation with reliable shutoff
Maintenance tracking Tag valves and link to account/CMMS Ongoing cycle Speedy parts ID and replacements

Proper handling and commissioning extend service life and keep the Resilient Seated Gate Valve looking and working like new.

Work with Me at Yaxing Valve to Specify the Right Iron Gate Valve Today

Contact me with your line size, pressure expectations, and flow needs and I will match the exact series and type to your duty range and temperature limits.

My concise checklist speeds approvals: end type, inside-screw vs non-rising, and handwheel orientation. I also note stem handwheel and screw details for clear install guidance.

See the gallery for high-res images and layout views that show clearance and operator reach. Make an account to save specs, tag valves, and link drawings plus a one-page field PDF.

Ask for a quick quote and I’ll confirm availability, lead times, alternates, and help you complete the order while you view the gallery. I use cookies only to keep your account session and cart ready.

AMT Endoscopy for ENT Specialties

AMT’s Endoscopy Services in Singapore Explained.

“The important thing is not to stop questioning.” — Albert Einstein.

AMT’s endoscopy integrates precise manufacturing with clinical care. We will explore how AMT connects device manufacturing to supporting gastrointestinal procedures in Singapore.

Accuron Technologies lately took a strategic step with AMT endoscopy. By placing Aurum Healthcare under Advanced Materials Technologies. They also added sterilization and cleanroom capabilities in Johor Bahru, expanding AMT’s presence in Tuas and Dongguan. Thanks to this, AMT can now handle end-to-end production from precision parts to sterile assembly.

You’ll discover why AMT’s endoscopy services are important for hospitals, device makers, and patients. Topics include manufacturing technologies and cleanroom services. Coverage includes partnerships, how endoscopy is used, safety rules, the costs, training for the workforce, and new trends like AI, robotics, and making things smaller.

Singapore enables medical tourism in the region, making AMT’s endoscopy services important for Southeast Asia. Next we explore the technologies and clinical uses that keep modern medical endoscopy both effective and able to grow.

Where AMT Fits in Singapore’s Endoscopy Ecosystem

Advanced Materials Technologies (AMT) is a specialist in Singapore for making precision metal parts. Core strengths include metal injection moulding and additive metal manufacturing. AMT focuses on urology, endoscopic devices, and surgical robotics and meets the needs of global brands seeking top-notch components.

How AMT Strategizes

Accuron Medtech accelerates growth in the Asia-Pacific medtech scene, sharpening AMT on medical devices. Its teams specialize in design-for-manufacturing across additive and MIM processes needed for top-tier endoscopy products.

Scale Through Targeted Additions

Aurum’s acquisition expanded AMT with validated cleaning and assembly. Aurum Healthcare’s Johor Bahru facility expanded AMT’s capacity and scope, allowing delivery from metal parts to sterilization and plastic assembly.

AMT - endoscopy

Support for OEMs & Robotics

AMT enables endoscopy device makers with precise parts and cleanroom assembly. Services span designing to validating sterility, speeding up launches while improving quality and cost control.

By linking component production with cleaning and assembly, AMT is a strong partner for endoscopy and surgical robotics OEMs, simplifying programs, speeding validation, and readying advanced tools for surgery.

What “AMT’s Endoscopy” Covers—and Why It Matters

This section outlines AMT’s role in healthcare and device making. “AMT’s endoscopy” means the parts and services AMT provides for endoscopic procedures—from high-precision metal components to cleanroom-assembled and sterilized tools used in clinical settings.

Definition in device production and clinical procedures

AMT produces precise metal parts via MIM and 3D printing, and manages cleanroom assembly, sterilization, and tracking for clinical use. These sterile, validated parts are essential for safe endoscopy.

Manufacturing vs Clinical Services

AMT owns engineering, quality control, regulation, and production—but does not clinical care. Hospitals and clinics conduct procedures using AMT’s parts, maintaining a clean division of responsibilities.

Regional Value of Singapore’s Medtech Hub

Singapore combines advanced manufacturing, robust regulation, and top clinical centers, helping OEMs rapidly move designs to market. Local supply and services make Singapore an important location for medical endoscopy and draw regional patients.

  • Faster prototyping and supply for regional hospitals and endoscopy networks
  • Strong quality controls meeting export and local clinical requirements
  • Tighter OEM-clinician feedback loops to refine devices

Understanding the line between AMT’s manufacturing and hospital services demonstrates how the ecosystem drives better care, aiding doctors and enabling device companies to expand innovation.

Advanced endoscopy technology produced and supported by AMT

AMT produces key components for advanced endoscopy used in Singapore and by regional OEMs, combining conventional metal forming with modern processes to meet high standards.

MIM & Metal Additive

AMT specializes in small, strong parts—joints, tips, housings—via MIM, and uses 3D printing for complex shapes hard to make otherwise, enhancing assembly and ensuring reliability.

Sterilization, Clean Assembly & QA

AMT provides audited sterilisation and clean assembly with ISO-aligned systems, including trackability for consumables and plastics, supplying catheter and disposable needs while remaining compliant.

Miniaturization trends and imaging demands

As parts shrink, e.g., camera housings, AMT meets precision demands where imaging and therapy converge—delivering tiny, durable components for modern scopes.

Key benefits are fewer parts, reliable performance, and easier sterilisation checks—speeding development and enabling better diagnosis and therapy.

Procedures Using AMT-Supplied Components

GI endoscopy spans diagnostic checks to complex interventions. Device makers require tough, exact metal components and re-sterilizable tools—AMT supplies both manufacturing and sterile assembly to Singapore hospitals.

Diagnostic: Gastroscopy, Colonoscopy, Video Scopes

Diagnostic scopes employ imaging and biopsy features; video endoscopy needs rigid, robust housings. AMT provides tip components and biopsy forceps parts, maintaining image stability and device reliability.

Biopsy tools are sterilized and tracked; reliable components reduce downtime and enable AI-assisted workflows.

Therapeutic: Polypectomy, Hemostasis, EMR

Therapeutic tools—snares, cutters—require heat- and stress-resistant precision. AMT’s fabrication delivers precise snare wires and cutters, with sterile lines preparing them OR-ready.

Interventional and hybrid procedures enabled by advanced components

Hybrid approaches combine endoscopy with other techniques, demanding specialized components. AMT enables navigation and robotic integrations via dependable designs and strict sterile processes.

  • Scope tip assemblies for video endoscopy and gastroscopy
  • Precision snares and cutters for therapy
  • Articulated connectors for interventional work

Clinical benefits of minimally invasive endoscopy and diagnosis

Minimally invasive endoscopy has upgraded patient care in Singapore—faster recovery and lower risks. With tiny tools and advanced optics, doctors operate through small access points, cutting hospital time.

AMT specializes in precision parts and sterile items clinicians rely on for everyday care.

Reduced sedation, faster recovery and patient comfort

Lower sedation is safer for the elderly and comorbid patients, allowing quicker discharge. Ergonomic devices and miniaturized parts make procedures gentler, boosting acceptance.

One-Session Diagnose-and-Treat

Modern scopes enable diagnosis and therapy in a single visit, cutting risk and cost while enhancing convenience.

Sharper Imaging with AI Support

High-definition imaging shows finer details; AI adds real-time analysis. Well-engineered optics and mechanics enable early detection and better planning.

  • Sharper optics and stable mechanics keep images AI-ready
  • Advanced manufacturing keeps optics aligned and protected
  • Validated sterile workflows lower infection risk

Workforce & Training Around AMT

Singapore’s endoscopy teams combine clinical expertise and technical skill, supported by hospitals, national programs, and industry partners to maintain high quality.

Skills Needed for Advanced Endoscopy

Advanced techniques demand precision and device fluency—EMR, polypectomy, hemostasis—plus cross-disciplinary learning with robotics and AI. Simulators and structured assessments translate knowledge safely; device literacy lowers risk.

How Providers and OEMs Upskill Teams

Major hospitals offer specialized training and continuing education. Manufacturers deliver device use, care, and maintenance training for clinical understanding.

Combining courses with Singapore’s initiatives and OEM input creates a well-rounded learning path.

Expertise Hubs & Access

Expertise concentrates in large centers, improving complex case outcomes and training, but limiting smaller sites. Regional patients travel to Singapore for specialized care, underscoring its hub role.

Outreach, tele-mentoring, and broadened training can help spread excellence and reduce gaps.

From Referral to Recovery in Singapore

At Singapore endoscopy centers, the journey goes from referral to recovery with defined steps, including minimal-sedation or awake options.

Before the Procedure: Steps

Pre-procedure checks assess history, medications, bleeding risks, and fasting. Teams explain benefits and risks with plain consent forms; many sites offer same-day pathways to cut waiting.

OR Standards, Sterilisation & Cleanroom Impact

Clean theatres and validated instrument flows are essential. Integrated sterilization, assembly, and device supply improve safety and tighten tracking of single-use items.

Documented workflows lower infection risk and ensure standards are met; working with one provider often speed supply and shorten chains.

Post-procedure care, follow-up and national integration

Post-procedure care centers on recovery, complication watch, and results communication. Linking with national records enables follow-ups and device traceability from manufacturer to patient.

Governance for Endoscopy Devices

In Singapore, endoscopy devices adhere to high standards. The Health Sciences Authority oversees registration, documentation, and post-market safety before clinic use.

Singapore’s Medtech Regulatory Landscape

Hospitals and suppliers demonstrate HSA compliance via risk management, clinical evidence, and quality checks. Global standards are referenced approvals for proven devices.

Quality, Sterility and Tracking

Quality systems follow ISO frameworks. Sterilisation uses validated methods to assure sterility. AMT’s traceability tracks each device from build to use for rapid responses if needed.

Governance & Surveillance

Hospitals monitor performance and escalate issues via registries. AMT’s documentation aids clinicians and OEMs in resolving problems; oversight expands with smarter devices to cover data and responsibilities.

Costs, Economics & Access

Advanced endoscopy is not cheap for providers and patients—high-end scopes and robotics carry large capital costs plus maintenance contracts.

Costs increase with complex imaging and AI requirements. Where makers also manage sterilization and parts, costs can drop via integrated supply.

Training and dedicated spaces remain costly, affecting price. Large centers absorb costs better than smaller sites, influencing access.

Medical tourism brings revenue yet may shift focus toward premium services, raising equity questions.

Leaders explore shared buying and partnerships to balance fairness with innovation.

Innovation: AI, Imaging & Next-Gen Surgery

Rapid advances transform clinician-manufacturer collaboration in Singapore and the region. AMT’s supply chain links precision manufacturing with clinical needs for performance and safety.

AI-assisted detection aids spot subtle lesions, relying on stable feeds and reliable equipment so algorithms identify issues in real time.

AI Governance come with AI adoption—testing for fairness, data handling, accountability, and consent are addressed across makers and providers.

Navigation & Integration update surgical precision via overlays, articulation, and robotics, where OEM-manufacturer coordination meets strict thresholds.

  • Robotics improve reach and stability
  • Navigation pinpoints tricky targets
  • Combining modalities reduces re-interventions

Going Smaller drive tiny cameras and instruments that demand advanced metalwork and careful assembly able to endure reprocessing while keeping clean views for AI.

Data-Driven Procedures improve records and analytics but raise questions on ownership, use, and privacy—calling for clear rules for storage, sharing, and study.

Together, these trends make surgery more accurate and data-guided, requiring strong ties among design, manufacturing, trials, and regulation to keep care safe and effective.

Regional Impact & Strategy

AMT’s combination of metals, sterile plastics, and assembled devices—enhanced by Aurum—lets Southeast Asian hospitals access advanced tools quickly, reducing wait times for endoscopy by amt procedures.

AMT strengthens Singapore’s medtech hub status, attracting APAC firms, speeding development, and spurring investment. With Accuron and AMT growing, Singapore’s global health role rises, supporting medical tourism and regional ties.

Challenges remain: elevated costs and specialized skills can limit access. AMT eases supply bottlenecks, but equitable policies remain crucial so benefits reach all.

By integrating MIM, 3D printing, and sterilisation, AMT provides Singapore an edge, drawing outsourcing and helping broader access to tools like endoscopy by amt, supporting both economy and public health.

FAQ

What does “AMT’s Endoscopy Services in Singapore” refer to?

It refers to AMT’s manufacture and supply of endoscopy tools: metal parts via printing and molding, plastics, cleanroom assembly, sterilization, and tracking—ensuring devices are hospital-ready.

Who Is AMT and What Can They Do?

AMT is a Singapore manufacturer of precise medical parts using MIM and metal printing for areas like endoscopy; with Accuron’s medtech focus, AMT supports DFM and component supply across APAC.

AMT’s Path to Sterile Assembly

Through Aurum Healthcare—brought under AMT via Accuron—adding Johor Bahru capabilities and China support to complement Singapore, enabling end-to-end manufacturing to sterile prep.

How Does AMT+Aurum Help OEMs & Robotics?

One-stop path to precision metals and plastics, cleanroom assembly, and sterilisation speeds launches, strengthens traceability, reduces quality risk, and manages costs under unified QA.

Clinical Service Scope

No. AMT supplies parts and assemblies; hospitals and specialists deliver patient care. AMT focuses on devices.

Endoscopic Components from AMT

Tiny housings, tip components, forceps elements, snares, cutters, and linkages via MIM and metal printing for reliable procedures.

Why Additive & MIM Matter

They enable intricate, miniaturized parts, simplify assembly, ensure quality, and meet higher imaging and precision needs.

How Quality and Sterility Are Ensured

Validated sterilisation, cleanroom assembly, tracking, and ISO-aligned QA with records to satisfy safety and regulatory needs.

Procedures Using AMT Components

Diagnostics like gastroscopy, colonoscopy, video endoscopy; therapies like polypectomy and hemostasis—which require precise and sterile tools.

Advanced Procedure Support

Yes—custom metal parts and cleanroom workflows for complex procedures with robust designs and strict sterility.

Impact on Patient Experience & Workflow

Smaller, ergonomic tools reduce discomfort and speed recovery; reliable devices support comprehensive single-session care and lower risk.

Training & Workforce Implications

More advanced tools require robust training across hospitals, programs, and OEMs using simulators and device guidance for safe adoption.

Patient Journey Overview

Referral, assessment, consent, often outpatient flow; suppliers like AMT ensure tools are sterile, reliable, and available throughout care.

Regulation & AMT’s Services

Compliance with HSA and international standards—sterility, QA, and tracking—keeps devices safe and compliant with monitoring rules.

How do traceability and validation reduce patient risk?

End-to-end tracking and validated sterilisation allow fast issue response and reduce infection risk, supporting hospital safety.

Why Advanced Endoscopy Costs More

Premium scopes, robotics, imaging, and AI contribute to capital and upkeep; integrated providers like AMT help lower waste and streamline supply.

Access Implications of Integration

One-stop models can lower total cost for hospitals, but skills, space, and capital needs nevertheless limit access, tilting toward major centers.

What role does Singapore’s cluster play regionally?

Quality manufacturing, regulation, and clinics draw patients and investment; AMT expands regional tool access while equity stays a focus.

AMT & AI Imaging Stability

Precision builds and clean assembly keep optical stability so AI can reliably analyze frames effectively.

Next-Gen Modalities with AMT

Providing complex, precise parts to endoscopy and surgical OEMs enables integrated, regulated, and sterile next-gen procedures.

Future Trends Shaping AMT

Miniaturization, AI-rich imaging, and more robotics grow demand for precise parts and sterile consumables; AMT’s breadth helps faster client development.

After-Market Governance Support

Records, traceability, and QA data enable incident reporting, corrective actions, and long-term compliance across hospitals and OEMs.

Equity & Policy Considerations

While AMT improves supply, training and cost gaps remain; regional policies should promote affordability and access as technology advances.

Ribbon Splitting and Recombining in Lines

FTTH Cable Production: Manufacturing Process Explained

Surprising fact: over seventy percent of new broadband deployments in the U.S. now rely on fiber networks that require high-precision manufacturing to achieve required performance.

Shanghai Weiye OFC Equipment runs full-cycle SZ stranding line manufacturing, from sourcing brand fibers like Fujikura or Corning SMF-28e to comprehensive test documentation that guarantee full quality assurance.

Our drop cable designs suit overhead, underground, and direct burial installation, with LSZH, PVC, and polyethylene (PE) jacket options and configurations from 1–4 cores. We offer single-mode OS1/OS2 and multimode OM2–OM4 grades plus G.652D and ITU-T G.657 variants, Pantone sheath colors, and custom logo printing.

Automation and high-precision equipment keep line speed steady and keep repeatability high. Typical lead times are four to five days for orders under 100 km and 7–10 days for < 500 km, with an min. order of 1 km and warranty covering free replacement for confirmed quality issues.

Continue to understand how materials, testing, and support combine to lower lifecycle cost and match the right product to your network system.

  • Shanghai Weiye OFC Equipment provides end-to-end manufacturing and lab testing for United States projects.
  • A range of jacket options and optical grades cover different install environments.
  • Automated production lines ensure stable quality and reliable optical performance.
  • Quick lead times, low MOQ, and brand fiber options support reliable procurement planning.
  • Comprehensive test reports and warranty back product reliability and compliance documentation needs.

Specialized FTTH Manufacturing by Shanghai Weiye OFC Equipment

When project timelines and performance matter, Shanghai Weiye OFC Equipment delivers customized drop cables with full test documentation.

As a dedicated manufacturer, Shanghai Weiye OFC Equipment pairs purpose-built equipment with stringent material control. We provide customized service and products for residential/MDU deployments. Every order includes full QA coverage and full test reports.

Our lab runs high heat, salt spray, and vibration tests to verify durability. Jacket options cover LSZH, PVC, and PE. Designs cover bow-type flat and self-supporting styles and support brand fibers such as Fujikura and Corning SMF-28e.

FTTH cable production line

  • Controlled production lines and production checks for fully auditable shipments.
  • Engineering support for specification reviews, trials, and volume ramp.
  • Modern fixtures and calibration minimize variation so every cable matches operator specs.

How We Produce FTTH Cable

At Shanghai Weiye OFC Equipment, manufacturing steps are matched to network specs, combining brand fiber choices with rigorous test routines.

Fiber Selection & Brand Options

We match Fiber coloring machine to minimum bend radius, attenuation, and deployment type. Options include OS1, OS2, OM2–OM4 and ITU-T G.652D, G.657.A1/A2. Brand fibers such as Fujikura® and Corning SMF-28e are available to satisfy sourcing standards.

Strength member integration

Strength members employ FRP (dielectric) or galvanized steel wire. FRP is preferred where non-conductivity is necessary. Steel wire provides tensile strength for long-span aerial runs and bonding/grounding needs.

Jacket extrusion and process control

Jacket options include LSZH for flame/smoke safety, PVC for flexibility, and PE for outdoor UV and moisture resistance. Tight process control of temperature and capstan ratios stabilizes line speed and critical dimensions.

Component Dielectric FRP Steel wire
Use case Electrical isolation High-tension aerial runs
Advantage Lightweight, inert Very high tensile strength
Installation note Simple terminations Requires grounding

In-Process and Final Testing

Inline geometry/concentricity checks operate in-line. Final optical tests confirm loss and return loss. Each order ships with a full test report and lab results from high-temperature, salt fog, and vibration tests to qualify field handling and drop terminations.

Typical lead times are 4–5 days for < 100 km and under 500 km in 7–10 days. Material lot records and FAI approvals support traceability and compliance for U.S. projects.

Our FTTH Drop Cable Types and Structures

Shanghai Weiye OFC Equipment offers a compact portfolio of drop designs that suit both tight indoor routes and exposed aerial spans. Each option pairs tested materials with geometry tuned for field termination and consistent optical performance.

The bow-type flat drop cable minimizes footprint for risers/ducts. It reduces bend loss for easy routing in hallways and MDUs.

Self-supporting designs for aerial spans

Self-supporting FTTH drop designs use a messenger element to carry tensile loads. Choose dielectric FRP for electrical isolation or steel wire when bonding and higher tensile strength are required.

Layouts & Strength Members

We offer dielectric and metallic strength member configurations to meet safety/EMI requirements. Center loose tube and flat unitube types balance crush resistance and fiber secondary coating line for quick termination.

Indoor/outdoor jackets

Jacket choices include LSZH for flame-retardant, low-smoke indoor use and PE for outdoor UV and moisture resilience. Each series is validated for mechanical and optical quality before shipment.

Type Application Strength element Sheath
Flat bow-type Indoor risers, MDUs Dielectric FRP LSZH
Self-supporting (aerial) Aerial spans FRP/Steel Polyethylene
Center loose tube Higher-count builds Dielectric FRP LSZH or PE
Flat unitube Low count, quick strip FRP or steel LSZH/PE

Production Assets for Speed and Quality

Automation and sensor-driven feedback at Shanghai Weiye OFC Equipment cut manual handling and increase throughput for drop patch preparation.

Our production line uses automated machines that cut/strip drop cords to increase output and reduce operator variability.

The CLX-BPO2 automated stripper runs under PLC and photoelectric control. One cycle is about 1.5 seconds, giving ~20 terminals per minute in production.

Automated Cut/Strip for Drop Cords

The equipment strips LSZH/PVC jackets and trims FRP/steel members to precise stub lengths. Cylinder-driven actuators provide quick, repeatable motion and low downtime.

PLC & Photoelectric for Precision

PLC logic and photoelectric sensors deliver precise positioning and feedback control. Inline checks feed control charts so operators can adjust drifts before out-of-control conditions occur.

Item Spec Benefit
CLX-BPO2 1.5s cycle, auto-strip High throughput
Actuation Cylinder-based High speed and reliability
Materials LSZH & PVC; FRP & steel Accurate stubs, clean terminations
Control PLC + photoelectric + inline checks Consistent quality, lower rework
  • Automated waste ejection and ergonomic loading keep the line clean.
  • Process control plans document calibration and key parameters.
  • Integrated assets and trained operators help meet FTTH volume goals without compromising accuracy.

CLX-BPO2 auto-stripping machine capabilities in our line

The CLX-BPO2 provides industrial-grade strip/trim to our line, cutting cycle time while maintaining consistent prep.

Shanghai Weiye OFC Equipment deploys the CLX-BPO2 to increase throughput and standardize terminal quality. The unit runs at an approximate cycle time of 1.5 seconds, producing around 20 preps per minute in production.

PLC/photoelectric control deliver exact detection and repeatable motion. That control keeps strip and stub lengths within tight tolerances.

Line Speed

Typical operation speed is 1.5s per cycle. This enables steady throughput under continuous line conditions.

Supported jacket and reserved strength lengths

The CLX-BPO2 handles LSZH/PVC with an adjustable strip length from 17.5 to 35.0 mm. Reserved stubs are set between 7.0 and 11.0 mm to fit common termination hardware.

Handling FRP and steel wire strength members

The machine cuts FRP/steel strength elements cleanly while protecting adjacent fibers. Custom tooling are offered for non-standard cross-sections to maintain precision.

  • Auto-eject scrap and sensor start cut idle time.
  • Small footprint (L40 × W18 × H18 cm), 50W at 110–220V, and 11 kg weight simplify cell integration.
  • Pneumatic cylinders and closed-loop control improve line reliability and lower maintenance interruptions.
Specification Value Why it matters
Cycle time ≈1.5 s (~20/min) Supports high-volume runs
Jacket strip (A) 17.5 to 35.0 mm Compatible with common connectors
Reserved stub (B) 7.0 to 11.0 mm Meets strength and termination needs
Power & size 50W @ 110–220V; 40×18×18 cm Simple integration

Using this machine, Shanghai Weiye OFC Equipment standardizes terminal prep so field teams receive drop parts ready for quick installation. The CLX-BPO2 helps our production lines meet volume goals without sacrificing quality.

Customized specifications to fit your FTTH system

Shanghai Weiye OFC Equipment configures each build to fit your network requirements and simplify deployment. We pair concise options with predictable manufacturing windows so your teams get install-ready reels.

Choose 1–4 core designs with SM or MM fiber. Options include OS1/OS2 plus OM2–OM4 along with G.652D and G.657 variants to match your optics and connector plans.

We match sheath colors to Pantone codes for quick field identification and consistent asset tagging.

Jackets, Legends & Branding

Select LSZH/PVC/PE jackets to suit route and safety requirements. Custom legends/logos support inventory and warranty tracking.

Lengths, Packaging & Special Builds

Standard reel lengths are 1/2/4 km with tailored reels and packaging to fit storage/handling. Choose bow-type flat or self-supporting designs and FRP or steel members to fit span and isolation requirements.

Option Common choice Benefit
Length 1, 2, or 4 km Less staging, easier reels
Sheath LSZH, PE, PVC Indoor/outdoor compatibility
Structure Flat bow / Self-supporting Routing and span flexibility

As a supplier, Shanghai Weiye schedules runs to your plan and provides docs that lists final specifications for straightforward QA on site.

QA, Testing & Documentation

Shanghai Weiye OFC Equipment embeds quality checkpoints across the production line so every item has recorded acceptance data at ship.

Environmental and Mechanical Tests

Our lab conducts high-temperature exposure, salt fog corrosion, and vibration tests to qualify materials and assemblies. These tests simulate field stresses for indoor and outdoor use.

Full Test Reports for Every Reel

Every fiber optic cable includes a 100% test report that records loss, return loss, and key geometry where applicable. Final QC gates prevent nonconforming shipments before they leave the factory.

Traceability & Compliance

Batch records link tests to reels/serials so audits and warranty claims are simple to verify. Documentation uses standard customer templates to accelerate approvals and receiving inspection.

  • Line checks and final inspection prevent field failures and lower warranty events.
  • Quality packages include specifications confirmation and formatted test data for rapid review.
  • Ongoing trend analysis inform preventive maintenance and raise long-term reliability.
Trial Purpose Result
High-temperature Thermal stability Validated heat endurance
Salt-fog Corrosion resistance Outdoor suitability
Vibration Mechanical robustness Improved field reliability

FTTH Drop Cable Pricing & Cost Drivers

Budgeting for a drop run starts with fiber and jacket choices and is shaped by volume and customization.

Typical prices range broadly—from about $30 to $1,000 per unit—based on fiber grade, jacket material, length, and structural design.

Primary Cost Inputs

The primary cost drivers are fiber grade, jacket material, and the structural type chosen for deployment.

Self-supporting structures and steel strength elements raise material and labor input. Custom colors, logos, and print legends add setup time and influence price for short runs.

Order length, volume, and customization impact on price

Longer put-ups and larger volumes lower unit cost. Short runs often include setup charges and higher unit prices.

  • Line changeovers and custom tooling extend lead time and add cost.
  • Clear RFQs and line scheduling let Shanghai Weiye OFC Equipment match quotes to delivery windows.
  • Frameworks and indexed pricing stabilize budgets over phases.
Driver Price impact Guidance
Optical grade Large Balance spec vs. budget
Sheath material Medium impact Compare LSZH vs. PE for total cost
Length/Volume High impact Consolidate runs to cut unit cost

Logistics for the U.S.

Shanghai Weiye OFC Equipment makes lead times and logistics clear so planners can align crews and sites. Predictable windows reduce downtime and control costs when a rollout is underway.

Scheduling & Capacity Planning

Typical production windows are 4–5 days for < 100 km and 7–10 days for orders under 500 km. We schedule line capacity to track your milestones and to maintain on-time delivery.

The service team provides updates/tracking so installation teams can plan arrivals. For tight schedules, we hold contingency capacity to accelerate critical-path orders.

Minimum order quantity and why it matters

The MOQ is one kilometer. This reflects setup needs such as wire/die adjustments that use startup material and generate scrap.

We review your length and staging plans to choose reel sizes that cut waste and handling. Batch releases can balance inventory holding with frequent, smaller deliveries to job sites.

Installation readiness and application scenarios

Site conditions dictate whether a self-supporting aerial, ducted pull, or direct-buried run is the best fit for a project.

Deployment Considerations

For aerial runs, Shanghai Weiye OFC Equipment recommends self-supporting designs with appropriate members to control sag and tension for long-term reliability.

Duct installations work best with low-friction sheaths and crush-resistant builds so pulling does not damage fibers. PE jackets are typical for underground and buried paths where moisture resistance matters.

Direct-buried designs require proper depth control per local codes and moisture-resistant jackets to protect the optic core over time.

Indoor Distribution and ONT

Indoor riser and plenum routes prefer LSZH to meet smoke/flame codes. Flat drop cable forms strip clean and present controlled strength stubs for quick ONT termination.

We advise on steel vs FRP (dielectric) strength members based on bonding requirements, lightning risk, and hardware compatibility. Standardized line prep shortens install time and minimizes scrap.

Deployment Key feature Field note
Overhead Self-supporting, steel or FRP Verify messenger hardware/tension
Underground duct Low-friction jacket, crush resistance Use pull tape and proper lubricant
Direct burial PE jacket, moisture barrier Follow local depth and warning tape rules
Indoor LSZH with tight-bend support Maintain bend radius at wall penetrations

Our approach delivers a consistent installation across indoor outdoor transitions. That leads to fewer callbacks, speeds activations, and reliable field performance for your system.

End-to-end support and after-sales service

Our team coordinates tests, line schedules, and installation guidance to avoid surprises in deployment.

Shanghai Weiye OFC Equipment provides engineering support from early requirements through approved drawings and pilot builds. We provide doc templates and clear install notes so field crews work from the same plan.

After-sales service includes fast response, RCA, and corrective action. All products ship with full reports and traceability to help QA acceptance.

  • Round-the-clock availability for status updates and technical guidance.
  • Warranty includes free replacement for confirmed quality issues.
  • Coordination of line schedules for expedites and urgent changes.
  • Configuration control so shipped items match agreed specs consistently.
Support area Scope Benefit
Engineering Spec review & pre-production builds Fewer field issues
Testing Lab trials & 100% test reports Full traceability
Service Fast replace + RCA Minimized downtime

Wrap-Up

Select Shanghai Weiye OFC Equipment for custom drops, quick lead times, and full traceability.

We provide custom FTTH drops that pair material choices with validated manufacturing and lab testing. Every reel includes a 100% test report and documented trials to support U.S. field acceptance.

A hardened production line, including CLX-BPO2-enabled prep machines, cuts variability and shortens turnaround. Our equipment set standardize strip/stub lengths so installers get consistent results at turn-up.

From fiber selection through jacket, printing, and packaging, we balance design and cost to extend service life. Dedicated support guides scheduling, logistics, and after-sales care so your deployment stays on plan.

Get in touch with Shanghai Weiye OFC Equipment to align specifications, timeline, and volume. We stand behind every shipment with laboratory validation and responsive support.

Related: Minimizing Delamination in Secondary Coating Lines

How China Injection Molding Reduces Production Costs

How to Secure Injection Molding Services with Chinese Suppliers

Well, the major meeting has just concluded. your new project has the green light, the timeline is aggressive, and the budget is, let’s say, constrained.. And suddenly someone—perhaps your superior or the finance head—says the fateful words that make any project manager’s heart skip a beat: “We should look at sourcing this from China.”

Of course, you acknowledge. It makes sense on paper. The cost savings can be huge. But your mind is already racing. You’ve heard the stories, haven’t you? The nightmare of defective parts, opaque communication, and delayed, off-spec shipments. It feels like walking a thin line between big savings and total project failure.

However, here’s the reality. Sourcing plastic mold company can be a calculated project. It’s a project, just like any other. And as with any project, success depends on your methodology. It isn’t about the cheapest offer but about choosing the right supplier and running the process transparently. Forget the horror stories. Let’s walk through a real-world playbook for getting it right.

China injection molding

First Things First: Your Homework

Before you even whisper the word “supplier” or open a browser tab to Alibaba, you need to get your own house in order. Honestly, more than half of all overseas manufacturing problems start right here, with a weak or incomplete information package. Don’t assume a remote factory can guess your needs. Sending a vague request is like asking a builder to quote you for “a house.” The replies will range from absurdly low to exorbitant, none of which help.

Aim to craft an RFQ package so precise and comprehensive it leaves no room for error. This package is your project’s foundation.

What should you include?

First, your 3D CAD files. They cannot be skipped. Stick to universal formats like STEP or IGS to avoid any compatibility headaches. This is the master blueprint for your part’s geometry.

But 3D isn’t enough. You also need detailed 2D drawings. This is where you call out the stuff that a 3D model can’t communicate. Examples include tolerances (e.g., ‘25.00±0.05 mm’), material grade, surface finish requirements, and functional callouts. Any seal surfaces or critical hole sizes must be clearly labeled.

Then specify the material. Don’t label it simply “Plastic.” Even “ABS” alone is too vague. Get precise. Call out SABIC Cycolac MG38 (black), for example. What’s the reason? Because resin grades number in the thousands. Defining the exact material guarantees the performance and appearance you designed with plastic mold injection.

A good supplier can suggest alternatives, but you need to give them a clear starting point.

Finally, include the business details. What’s your forecasted annual volume (EAU)? A supplier needs to know if they’re quoting a tool that will make 1,000 parts in its lifetime or 1,000,000 parts a year. Tool style, cavity count, and unit cost are volume-driven.

Hunting for the Best Supplier

Now that your RFQ is pristine. who will you target? The internet has made the world smaller, but it’s also made it a lot noisier. Finding suppliers is simple; finding quality ones is tough.

You’ll probably kick off on Alibaba or Made-in-China. They let you survey dozens of suppliers quickly. Use them to build a shortlist, not the final list. Narrow your pool to about a dozen promising firms.

But don’t stop there. Perhaps hire a local sourcing specialist. True, they charge a fee. But a good one has a vetted network of factories they trust. They bridge language and cultural gaps. For a first-time project, this can be an invaluable safety net. It’s schedule protection.

Also consider trade fairs. If you can attend, shows such as Chinaplas transform sourcing. Nothing beats a face-to-face conversation. Inspect prototypes, interview engineers, and sense their capabilities. Plus, ask peers for referrals. Ask other project managers in your network. A solid referral can be more valuable than any ad.

Shortlisting Serious Suppliers

With your RFQ dispatched to dozens of firms, bids begin to arrive. Some prices will undercut logic, others will shock you. Your task is to filter them down to 2–3 credible finalists.

What’s the method? It involves both metrics and gut feel.

First, look at their communication. Do they respond quickly and clearly? Do they communicate effectively in English? But here’s the real test: Are they asking you intelligent questions? Top vendors will critique and inquire. For instance: “Draft angle here could improve mold release. Tolerance check via CMM adds cost—proceed?” This is a massive green flag. It shows they’re engaged and experienced. A supplier who just says “No problem” to everything is a walking red flag.

Afterward, verify their technical arsenal. Ask for a list of their equipment. Seek samples or case studies of comparable projects. If you’re making a large, complex housing, you don’t want a shop that specializes in tiny gears.

Next up: the factory audit. Skipping this is a mistake. As you vet staff, you must vet suppliers. Either visit in person or engage a local audit service. They’ll send a local inspector to the factory for a day. They authenticate the firm, review ISO credentials, evaluate machines, and survey operations. It’s the best few hundred dollars you will ever spend on your project.

From Digital File to Physical Part

After picking your vendor, you’ve negotiated the price and payment terms—a common structure is 50% of the tooling cost upfront to begin work, and the final 50% after you approve the first samples. Then comes the real action.

Initially, expect a DFM report. Design for Manufacturability (DFM) is essential. This is your supplier’s formal feedback on your part design. The report calls out sink-risk zones, stress-causing corners, and draft angle gaps. A thorough DFM is a sign of a professional operation. It’s a collaboration. Together, you tweak the design for best manufacturability.

When you greenlight the DFM, they machine the mold. A few weeks later, you’ll get an email that will make your heart beat a little faster: “T1 samples have shipped.” These represent the first trial parts. It’s your test of success.

T1 parts usually require adjustments. That’s standard process. Look for small flaws, slight size errors, or surface marks. You’ll provide detailed feedback, they’ll make small adjustments (or “tweaks”) to the tool, and then they’ll send you T2 plastic mold samples. This process might take a couple of rounds. Plan for this loop in your schedule.

At last, you get the perfect shot. It matches all specs, has a pristine finish, and works as required. This becomes the “golden sample.” You formally approve it, and this sample is now the standard against which all future mass-produced parts will be judged.

Completing the Sourcing Journey

Getting that golden sample feels like the end, but it isn’t. Now you’re entering the mass production phase. How do you maintain consistency for part 10,000?

Implement a robust QC plan. Often, you hire a pre-shipment inspection service. Use a third-party inspector again. For a few hundred dollars, they will go to the factory, randomly pull a statistically significant number of parts from your finished production run, and inspect them against your 2D drawing and the golden sample. You receive a full report with images and measurements. After your approval, you release the shipment and final funds. This audit shields you from mass defects.

Lastly, plan logistics. Understand the shipping terms, or Incoterms. Is your price FOB (Free On Board), meaning the supplier’s responsibility ends when the goods are loaded onto the ship in China? Or is it EXW (Ex Works), where you are responsible for picking it up from their factory door? These details have a big impact on your final landed cost.

China sourcing is a long-haul effort. It relies on partnership-building. View them as allies, not vendors. Transparent dialogue, respect, and process discipline win. Certainly, it’s complex. However, armed with this guide, you’ll secure savings and keep high standards intact. You’re set to succeed.

Precious Metals Recycling for Precision Contact Assemblies

Eco-Friendly Precious Metal Recovery Handbook

More than $60 billion in precious metals end up in e-waste every year—did you realize that? Such a massive amount highlights why precious metal recycling is so vital. Recycling these metals benefits both the economy and the planet. When we recover gold, silver, platinum, and palladium, we reduce pollution and conserve resources.

Leaders such as Dongsheng Metal Trading are paving the way for sustainable recycling. They ensure these valuable metals are reused, not dumped in landfills. This precious metal recycling companies approach is key to eco-friendly recycling and sustainable practices.

Important Takeaways

  • Each year, e-waste discards over $60 billion in precious metals.
  • Recovering these metals cuts eco-impact and preserves resources.
  • Gold, silver, platinum, and palladium top the list of valuable metals.
  • Sustainable development depends on eco-friendly recycling.
  • Recycling experts like Dongsheng Metal Trading lead the industry.

What Makes Precious Metals So Valuable

Precious metals are rare, naturally occurring metallic elements that have captured the interest of investors and industries alike. Gold, silver, platinum, and palladium stand out for their distinct qualities. These include electrical conductivity, corrosion resistance, and substantial rarity. Extracting and refining them uses up huge resources, so recycling becomes critical.

precious metal recycling

The value of precious metals is influenced by market demand and the inherent qualities of each metal. Recycling precious metals plays a critical role in sustaining the supply chain. It also reduces environmental impacts associated with mining activities. Through exhaustive recycling processes, these metals can be restored to their original state. Such efforts save limited resources and create economic gains.

Defining Precious Metals

These metals’ special traits lend themselves to diverse applications. Their rarity and intrinsic properties are foundational to their economic significance. For example:

  • Gold: Prized for its shine and tarnish-proof nature.
  • Silver: Known for flexible uses and excellent conductivity.
  • Platinum: Renowned for strength and catalytic uses.
  • Palladium: Gaining traction in cars and electronics.

Benefits of Precious Metal Recycling

Recovering precious metals plays a crucial role in sustainability. It preserves resources and lessens the environmental cost of mining. Key benefits include:

  • Cutting down mining-related environmental harm.
  • Lower energy consumption compared to extracting new metals from the earth.
  • Supporting a circular economy via material reuse.
  • Opportunity for profit by recovering valuable metals.

The Importance of Precious Metal Recycling

Recycling precious metals offers substantial environmental and economic benefits. Emphasizing benefits helps cut environmental harm. It also drives economic growth and stability.

Green Benefits

The environmental benefits of recycling precious metals are significant. By reclaiming metals from discarded electronics and industrial scrap, we cut down on landfill waste. That cuts new mining needs and saves resources.

It curtails mining’s damage, like habitat loss and toxins. By prioritizing recycling, we work toward a greener tomorrow.

Financial Gains

Financial perks of recycling are just as strong. Using reclaimed metals trims manufacturing budgets. It lets businesses choose reclaimed over freshly mined metals.

It produces recycling-sector employment and strengthens markets with growing recycled-metal needs. Using these financial benefits, companies can improve profits. They add to a more sustainable marketplace.

Steps in Metal Recycling

The precious metal recycling process is complex, involving several stages to ensure maximum efficiency. It starts with collecting metals from various sources like discarded electronics, jewelry, and industrial scraps. Next comes sorting, cleaning, and testing to assess metal content and worth.

Recovery Steps

Such a methodical process ensures efficient recovery. Each step is designed to optimize the yield of precious metals. Sorting divides metals by kind and grade. Decontamination eliminates residues that block recovery. Chemical analysis pinpoints metal levels to drive technique decisions.

Recovery Methods

Cutting-edge processes boost precious-metal recovery. Thermal reduction applies intense heat to isolate metals. Melting refines and aggregates metals, while wet chemical processes are used for delicate separations. Recyclers like Dongsheng Metal Trading employ these approaches to improve yields and returns.

Types of Precious Metals that can be Recycled

Recovery efforts support both ecology and resource reclamation. A host of precious metals are recyclable, aiding markets and ecosystems. Knowing which metals are recyclable helps individuals and firms.

Key Precious Metals

Gold, silver, and platinum are well-known precious metals. They’re found in jewelry, coins, and industrial uses. Gold recovery is widespread because of its worth and need. Silver’s role in cameras, electronics, and solar energy makes its recycling vital.

Platinum, though less common, is valuable, mainly in catalytic converters.

E-Waste Metals

Electronic precious metals offer unique recycling chances. Gadgets—from phones to laptops—house palladium, indium, and more. Reclaiming them cuts e-waste and recovers key resources.

The need to recycle these metals is critical. Sectors strive to cut waste and boost recycling efficiency.

Industry Benefits of Precious Metal Recovery

Precious metal recycling is essential for several key industries, allowing them to use valuable resources efficiently and sustainably. Device manufacturing in electronics profits hugely from recovered metals. Aerospace and healthcare rely on them for vital parts. Examining industry recovery uncovers eco- and economic advantages.

Electronics Industry

Because devices abound with metals, electronics tops recycling efforts. Rapid technological advancements have led to a significant increase in electronic waste. Thus, recycling gold, silver, and palladium efficiently becomes vital. That saves resources and cuts mining carbon footprints.

Businesses enhance recovery to align with green and zero-waste aims. Such a move upholds efforts to conserve and protect.

Aerospace and Medical Equipment

Recycling precious metals matters for aerospace and healthcare, given their reliance on them. High-performance alloys are essential for manufacturing flight parts and medical devices due to their durability and resistance to corrosion. Recycling these metals can significantly lower material costs and comply with environmental regulations.

These sectors know green recovery eases resource shortages. And it improves operations, making metal recycling a smart green tactic.

Finding Precious Metal Recycling Companies

Locating reliable recycling partners ensures great results. It’s wise to ask important questions to understand their operations. Knowing their pricing and processing methods can greatly affect your experience. Service comparisons help you pick the best recycler.

Questions to Ask Recycling Companies

  • Which recovery certifications does your company have?
  • Can you explain your processing methods for different metals?
  • What are your recovery rates for various precious metals?
  • How do you handle pricing, and what additional fees might apply?
  • Can you provide references or testimonials from previous clients?

Evaluating Offers

You must evaluate services side-by-side to pick the right recycler. Create a table to compare key factors such as:

Company Name Recovery Rate (%) Processing Fee ($) Turnaround Time (Days)
Recycling Co. A 95 50 7
Recycling Co. B 90 45 5
Recycling Co. C 92 55 10

By comparing recycling services, you can find the best recycler for your needs. This ensures you get the most value and meet industry standards.

Precious Metal Recycling: Your Eco-Friendly Guide

Understanding how recyclers operate is key for those interested in precious metal recycling. They handle all stages, from gathering to final refining. Such management secures peak resource use and profit.

Recycler Operations

Recyclers use advanced methods for metal recycling, including testing, separation, and refining. Collection comes from devices, jewelry, and industrial waste. Then, they use sophisticated techniques to separate different metals. Finally, they refine each batch to recover gold, silver, platinum, etc.

That workflow both boosts recovery and promotes green methods. It’s fundamental to building a sustainable future.

Finding Your Perfect Recycling Partner

Key criteria matter when choosing a recycler. Begin by checking their green credentials. In today’s market, a commitment to sustainability is essential. Also, examine if they handle everything or only certain stages.

Your budget will influence your choice. Get quotes to compare different options. Firms such as Dongsheng Metal Trading tailor services to each sector. They remain a trusted partner for targeted recovery.

Types of Recycling Facilities

Metal recycling is a critical sector for sustainable practices and waste management. Multiple types of facilities handle various recycling demands. Understanding these facilities improves access to recyclers and their services. That supports firms and ecosystems alike.

Facility Categories

Metal recycling facilities vary widely in their operations. Some focus on precious metals, while others handle a wide range of materials. Common examples include:

  • Scrap yards process a broad mix of metal types.
  • High-value metal recyclers provide precision recovery for gold, silver, platinum, etc.
  • E-waste hubs target valuable metals inside tech devices.

Location and Access to Facilities

Accessibility to recyclers is key for efficient metal recovery. Firms need to plan transport logistics. Here are some factors that influence access:

Factor Description
Distance Closer sites cut shipping costs and delays.
Partnerships Strong ties with local centers streamline recovery.
Service Range Awareness of service menus aids in picking the right center.

Ultimately, facility type and access shape recycling success.

E-Waste Recycling & Metal Recovery

Electronic waste is a pressing issue in today’s world, causing environmental harm. Old gadgets hide valuable metals ripe for recovery. This highlights the importance of seeing e-waste as a valuable resource.

How Electronics Contain Precious Metals

Devices often contain bits of gold, silver, and palladium. You’ll find them in components such as:

  • Circuit boards
  • Connectors and ports
  • Capacitors and resistors
  • Battery terminals

From phones to TVs, electronics pack precious metals. Recycling lets us reclaim and repurpose those metals.

The Importance of E-Waste Recycling

Recovering e-waste metals safeguards the environment and reclaims materials. It reduces landfill waste and saves natural resources. The benefits of recycling e-waste metals are clear:

  • It minimizes environmental risks from improper disposal
  • It cuts down on carbon emissions through eco-friendly practices
  • It supports the circular economy by recycling materials back into production

Championing electronics recycling fosters responsible resource use. It secures a healthier planet for tomorrow’s children.

The Future of Precious Metal Recycling

Recycling is changing fast thanks to new tech and eco-driven demand. Facing resource limits, recyclers embrace new methods. By integrating novel processes, they pave the way forward.

Trends in Sustainable Recycling

Today’s sustainable recycling prioritizes waste reduction and low impact. Firms now use bio-packaging and low-energy methods. Such moves match worldwide green goals and nudge industries to be more eco-responsible.

Innovations in Precious Metal Recovery

New methods in recovery enhance recycling performance. Robotic sorting and chemical extraction raise recovery. They ramp up yields and shrink eco-footprints, advancing metal recycling.

Starting a Precious Metal Recycling Venture

Starting a precious metal recycling business demands meticulous planning and a deep grasp of operational and market dynamics. Leaders should map out steps, secure compliance, and set firm roots. That means in-depth market analysis and client identification. Permits and regulatory clarity underpin ongoing success.

Launching Steps

Setting up a precious metal recycling venture requires several essential steps:

  1. Conduct market research to understand needs and rivals.
  2. Create a comprehensive plan with objectives and tactics.
  3. Purchase the right gear for your recycling operations.
  4. Raise startup funds through financing or investors.
  5. Get all required permits and licenses.
  6. Deploy promotional plans to gain customers.

Compliance and Certifications

Knowing regulatory requirements is vital for a recycling startup. Meeting environmental rules protects your operation and the planet. Must-know compliance points:

  • Getting licensed by appropriate agencies.
  • Following all levels of waste and recycling regulations.
  • Certifying employee knowledge of safety and handling rules.

As a Final Point

Recovering precious metals conserves resources and protects our planet. It allows individuals and businesses to lessen waste’s impact on our planet. Recovered metals curb mining and fuel green-job growth in recycling.

Metal recovery delivers both eco and economic upsides. Partnering with companies like Dongsheng Metal Trading ensures a commitment to eco-friendly practices. That partnership bolsters circular models for recyclers and buyers alike.

A sustainable tomorrow hinges on our joint metal-recycling efforts. Raising awareness fosters mindful use and eco stewardship. Implementing these measures supports us today and safeguards future generations.

Minimizing Delamination in Secondary Coating Lines

Innovative FTTH Cable Production Line Apparatus Solutions

Did you ever consider the impact of rapidly growing internet cable demand on FTTH cable production technology? As our need for high-speed, reliable connectivity intensifying, industry leaders like HONG KAI and Nextrom are transforming the manufacturing landscape. They are unveiling innovative cable equipment to improve production efficiency. Not only does this shift cut operational costs but also upgrades high-speed internet cable quality, meeting today’s market standards.

Here, we’ll examine the groundbreaking equipment and methods reshaping Fiber coloring machine manufacturing. Discover how these innovations are ready to reshape the fiber optic sector.

Top Highlights

  • Understanding the importance of FTTH cable production line equipment in high-speed internet access.
  • Examining the significant role of companies like HONG KAI and Nextrom in driving technology innovation.
  • Learning the benefits of adopting next-gen cable equipment in manufacturing processes.
  • Recognizing how enhanced cable quality is critical for meeting consumer demands.
  • Appreciating the importance of production efficiency in a competitive market.

Grasping FTTH Cable Production Line Technology

The manufacturing of fiber optic cables, especially for FTTH technology, involves a intricate blend of state-of-the-art tools and exact methods. Modern production of these cables includes various components that improve efficiency and quality. Knowing these parts illuminates the progress toward next-level production systems.

Core Components of Modern Fiber Optic Cable Manufacturing

Today’s fiber optic cable making includes:

  • Extruder systems for coating and insulating fibers
  • Fiber tension control mechanisms to preserve optimal fiber quality
  • Automated operations that simplify production processes

These components work together to create a dependable and long-lasting product. For instance, advanced temperature control systems ensure consistent conditions. Automated adjustments also minimize human error.

Evolution from Traditional to Advanced Production Systems

The shift from traditional to automated systems marks a major leap in technology and methods. Earlier, manual methods have been replaced by automated systems. This change has resulted in:

  1. Higher productivity and shorter production times
  2. Reduced waste due to accurate material handling
  3. Better product quality thanks to stricter quality control

Key Technologies Driving Industry Innovation

Several core technologies are propelling innovation in the fiber optic field. These include:

  • Precision temperature control that regulates and maintains optimal production conditions
  • Automatic settings that adapt to changing production requirements
  • Advanced monitoring systems offering real-time feedback on production quality

Thanks to these technologies, manufacturers can guarantee their fiber optic products meet the stringent standards required for FTTH applications.

Essential Equipment for Fiber Secondary Coating Line Operations

In the world of fiber optic cable manufacturing, the fiber secondary coating line is key. It safeguards fiber optics through high-speed coating processes. As technology evolving, having the latest equipment is vital for optimal production and reliability.

High-Speed Secondary Coating Processes

Advances in secondary coating processes have significantly boosted manufacturing efficiency. Contemporary systems can now handle increased volumes, addressing rising demand. They apply coatings that boost durability and performance, resulting in top-tier fiber cable products.

Single and Dual Layer Coating Applications

It’s essential to differentiate between single and dual layer coatings in the fiber secondary coating line. Single-layer coatings provide basic protection, while dual-layer coatings deliver extra resistance to environmental stressors. Both methods employ high-speed processes for uniform coating application, ensuring fiber optics perform longer in various conditions.

Temperature Control and Curing Systems

Temperature control systems are vital for curing coatings during production. They maintain the right conditions for adhesive substances in the fiber secondary coating line. Accurate temperature management allows for ideal curing times and conditions, resulting in enhanced quality fibers ready for real-world use.

Fiber Draw Tower and Optical Preform Processing

The fiber draw tower is central in optical preform processing and cable manufacturing. It draws the preform into thin fiber strands, guaranteeing high-quality fibers with exceptional clarity and strength. The tower’s ambiance is carefully controlled to achieve precise dimensions and physical properties.

Optical preforms serve as the foundation of this process, shaping the fiber’s final characteristics. The preform’s quality affects light transmission and durability. Advances in preform manufacturing have improved Fibers in metal tube manufacturing efficiency.

Through advanced engineering and technology, the fiber draw tower and preform processing continue to evolve, meeting the growing demand for high-performance fiber optic cables. Excellence at the preform level yields better fiber optics, improving telecommunications and networking services.

Advanced SZ Stranding Line Technology for Cable Assembly

The SZ stranding line technology represents a major milestone in cable assembly, especially for fiber optic cables. It ensures precise stranding, critical for crafting top-tier cables that meet strict standards.

Precision Stranding Equipment Features

The core of the SZ stranding line is its precision stranding equipment, which boosts cable durability and reliability. Its key attributes include:

  • Advanced control systems that tweak settings in real-time for peak performance.
  • High-speed operation that boosts production efficiency.
  • Modular design for customization based on production needs.

Automated Tension Control Systems

Automated tension control systems are critical for maintaining consistency in stranding. They:

  • Guarantee uniform fiber tension and strength distribution along the cable.
  • Reduce defect rates, cutting down on waste and production costs.
  • Enable seamless integration of diverse materials, improving flexibility and performance.

Integration with Fiber Cable Sheathing Line

Integrating the SZ stranding line with the fiber cable sheathing line enhances production efficiency. This synergy enables for:

  • Streamlined workflows by minimizing manual intervention.
  • Consistent quality throughout the manufacturing process.
  • Higher throughput, addressing the growing need for superior cables.

Fiber Coloring Machine and Identification Systems

The fiber coloring machine is vital in telecom fiber cable production. It ensures each cable is identifiable and complies with color coding standards. Modern technology enables quick and precise color application, boosting manufacturing efficiency.

High-Speed Coloring Technology

State-of-the-art machines use high-speed technology for uniform and fast color application. This cuts production time without compromising quality. The machines’ precision secures accurate color application, aiding adherence to strict color coding standards, essential for smooth installation and maintenance.

Color Coding Standards for Telecom Fiber Cables

Color coding standards direct manufacturers and technicians in the telecom industry. They organize fibers for easy identification, reducing installation and troubleshooting errors. Each color denotes a specific function or fiber type, guaranteeing clarity in complex networks.

Following these standards, supported by fiber coloring machines, enhances safety and efficiency—a pillar of telecom operations.

Quality Control in Fiber Identification

Quality control is critical in fiber identification systems to satisfy market standards. Routine inspections during production check color accuracy and coding adherence. Advanced traceability systems track fibers, boosting product reliability.

This methodical quality control approach yields superior telecom fiber cable performance, satisfying both manufacturers and end users.

Specialized Solutions for Fibers in Metal Tube Production

The production of fibers in metal tubes is a specialized domain in modern cable solutions. This method enhances durability and environmental resistance of optical cables, making them ideal for demanding conditions. Specialized techniques encase fibers in metal, shielding them from damage and extreme environments.

In outdoor settings, where cables face harsh elements, these solutions prove their worth. Manufacturers have engineered advanced methods to fortify and ensure cable reliability, meeting the growing demand for durable communication systems. Precision Fiber coloring machine engineering and high-quality materials are integral in this process.

Employing specialized manufacturing methods ensures cables remain intact and reliable across industries. Companies emphasize innovative designs and robust materials to create top-tier optical cables for diverse environments and applications.

Fiber Ribbon Line and Compact Fiber Unit Manufacturing

The manufacture of fiber ribbons and compact fiber units is critical for modern telecommunication networks. This section explores the latest equipment and designs for these essential components. Innovators aim to meet the rising demand for dense cable solutions in data centers.

Advanced Fiber Ribbon Line Equipment

State-of-the-art fiber ribbon line equipment allows efficient production of high-quality optical fibers. It integrates the latest technology to produce compact fiber units with top performance, minimizing waste and improving throughput to suit various needs.

Compact Fiber Unit Design and Production

Compact fiber units are designed for space efficiency without sacrificing performance. Innovative methods shape these units for easy installation in diverse settings. These units are indispensable for data centers, addressing the need for dense cables that save space and accelerate data transfer.

High-Density Cable Solutions for Data Centers

High-density cable solutions are essential for modern data centers, enabling faster data transfer and greater bandwidth. These solutions often incorporate fiber ribbons, manufactured through advanced processes. As data usage surges, these cables underpin robust infrastructure to meet today’s digital demands.

Optimizing High-Speed Internet Cables Production

Efficient production of high-speed internet cables is fundamental for today’s networks. The quality of FTTH cabling systems drives reliable connections. Advanced manufacturing aims to boost performance while maintaining high standards.

Cabling Systems for FTTH Applications

FTTH cabling systems feature designs that improve signal transmission and cable longevity. They utilize premium materials and innovative engineering to deliver fast, dependable internet for users.

Quality Assurance in Fiber Pulling Process

The fiber pulling process is pivotal in cable production, requiring precise attention. Quality checks avoid damage and preserve signal integrity. Integrated monitoring systems ensure cable reliability and facilitate seamless installation.

Meeting Industry Standards for Optical Fiber Drawing

Adhering to industry standards in optical fiber drawing is vital for manufacturers. It secures production safety and cable reliability. Improving techniques and materials helps meet these standards, yielding superior cabling systems.

Final Thoughts

The evolution of FTTH cable production lines has transformed telecommunications, allowing manufacturers to produce high-quality, reliable cables for modern internet demands. As technology advances, adopting advanced manufacturing solutions is paramount to enhance production efficiency while upholding top standards.

With the rising need for strong infrastructure, companies must adopt innovative methods in their FTTH cable production. These modern approaches enhance cable reliability and promote sustainable manufacturing in the fiber optic sector.

To stay ahead in the fiber optic cable industry, embracing these advanced solutions is imperative. The future of cable production hinges on such innovations, ensuring telecommunications infrastructure can meet the growing global internet demands.

Related: Ribbon Splitting and Recombining in Lines